System Integration & Control Systems Design


Control loop: Case History 141 - Report after optimisation exercise - Part 2

April 2015 System Integration & Control Systems Design

The first part of a report, published in Case History 140 (February), showed successes obtained and problems uncovered in an optimisation exercise in a particular process plant that takes optimisation very seriously. The plant has benefited both financially and from a productivity point of view, by ensuring that their base layer controls are running properly. As mentioned, this report was circulated to other relevant departments including C&I maintenance, process engineers and management.

Example 1 – proper tuning solves the problem

The first example in this second article is of a success story. Production was complaining that the control of a level in a particular drum was extremely poor. Tight level control is needed and it is vital that the level stay as closely as possible to setpoint under conditions of frequent load changes.

The figures shown here are done by an accurate simulation, as it is much easier to see what is happening than by looking at the original graphs, which were very noisy.

The level control consists of a normal flow-level cascade. The flow control was working well, and the problem was found to be with the tuning. Levels are generally integrating type processes, which are difficult to tune if one doesn’t understand how they work, particularly on long retention time vessels, which is the case with this particular process.

Figure 1 shows the response to a 5% step change in setpoint. The original tuning was P = 0,8, and I = 24,5 minutes/repeat. It can be seen that it took the level nearly 2 hours to move the 5% and get the PV to the new setpoint! One can see why the operators were complaining of bad control performance. There is no way this control could effectively catch load disturbances.
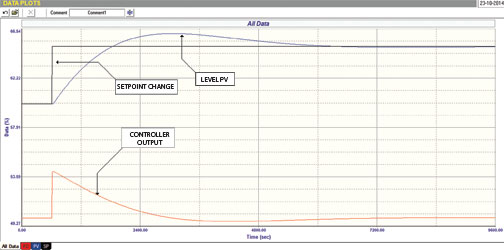
Figure 1.
Figure 1.

The controller was retuned to P = 8,0, and I = 11,0 minutes/repeat. The response to a 5% setpoint change is shown in Figure 2. The response time to move the 5% is now only about 15 minutes, some 8 times faster. This type of performance can be critical in effective production of complex processes.
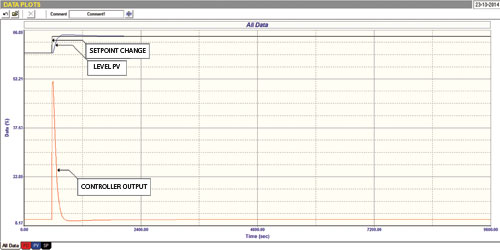
Figure 2.
Figure 2.

Example 2 – non-linearity and poor design make for an impossible situation

The second example in this article is of a major problem with the temperature control of the desuperheater on a boiler. This is a critical control as it controls the temperature of the steam, and can affect all sorts of processes in the plant that use the steam, particularly in distillation processes. The actual control is the secondary of a temperature to temperature cascade on the desuperheater. This is the control that actually operates the spray water cooling valve.

Strangely enough, even though there was a flowmeter measuring the flow of water through the valve, this was not cascaded to this temperature control which is the sensible thing to do.

The control was not working well and was running in manual, causing much aggravation and difficulty for the operators, let alone the effects on production. Figure 3 shows an open loop test which was performed by making step changes on the output of the controller, and observing the valve response by recording the flow through the valve.
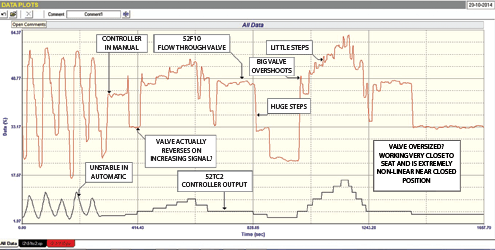
Figure 3.
Figure 3.

The test shows that the valve is really bad with respect to the following:

• It appears to be hugely oversized and controller output is working very low down which suggests the valve is almost closed. There is tremendous non-linearity in this region causing instability in automatic.

• The valve is sticky, and it sometimes moves the wrong way and it also has large overshoots on stepping.

There is no way that good control can be achieved with this valve. The valve should be used in cascade flow control to the temperature controller – this will go a long way towards solving the problem.

Michael Brown is a specialist in control loop optimisation with many years of experience in process control instrumentation. His main activities are consulting, and teaching practical control loop analysis and optimisation. He gives training courses which can be held in clients’ plants, where students can have the added benefit of practising on live loops. His work takes him to plants all over South Africa and also to other countries. He can be contacted at Michael Brown Control Engineering cc, +27 (0)82 440 7790, michael.brown@mweb.co.za, www.controlloop.co.za


Credit(s)


Share this article:
Share via emailShare via LinkedInPrint this page

Further reading:

How certified industrial automation channels become co-creators in the AI era
Schneider Electric South Africa System Integration & Control Systems Design
As industrial automation becomes software-driven and AI-enabled, the role of channel partners is shifting from equipment supply to outcome-based consulting, software integration and lifecycle services that require continuous certification and capability development.

Read more...
Why integration defines the next competitive edge in pulp and paper
System Integration & Control Systems Design
ABB’s Arvin Ramjee argues that fragmented automation, assembled from different suppliers at different stages of a plant’s lifecycle has become one of the pulp and paper industry’s most overlooked commercial risks, and that true integration, rather than surface-level connectivity, is what delivers measurable business value.

Read more...
Integrated automation enhances water treatment at dairy facility
Process Dynamics System Integration & Control Systems Design
Process Dynamics delivered the electrical, instrumentation, control and automation integration for an advanced water treatment and reverse osmosis system at a major South African dairy processing facility, achieving a 50% reduction in the client’s water utility costs.

Read more...
Intelligent process control is reshaping cement production in Africa
System Integration & Control Systems Design
Advanced process control, predictive analytics and automation are helping African cement producers cut energy use and stabilise output as they contend with rising electricity costs and tighter margins.

Read more...
Schneider Electric’s Alliance Programme turns system integrators into trusted technology partners
Schneider Electric South Africa System Integration & Control Systems Design
: Schneider Electric’s Alliance Partner Programme is helping system integrators across Africa move beyond one-off projects and build the skills and service models needed to become long-term industrial technology partners.

Read more...
Process Dynamics – Integrated Automation for Dairy Water Treatment
Process Dynamics System Integration & Control Systems Design
   Project and industry Process Dynamics delivered the electrical, instrumentation, control and automation integration for an advanced water treatment and Reverse Osmosis (RO) system at one of South Africa’s ...

Read more...
New SI programme strengthens Schneider Electric’s partner ecosystem
Schneider Electric South Africa System Integration & Control Systems Design
Schneider Electric’s SI Energise 2.0 programme offers system integrators a competency-based framework to develop deeper expertise in EcoStruxure and AVEVA software, enabling them to deliver full-lifecycle industrial automation solutions.

Read more...
AI and smart solutions for underground proximity detection systems
System Integration & Control Systems Design
Booyco Electronics explains why fitting proximity detection systems underground is far more complex than installing sensors, and how integration, data and intelligent analytics are helping mines manage the challenge.

Read more...
Why cloud-ready BMS is reshaping building operations
Schneider Electric South Africa System Integration & Control Systems Design
Smart sensors and non-contact radar are reshaping industrial measurement, feeding connected platforms that predict failures before they happen.

Read more...
Flotation system modernisation for a gold processing and mineral recovery plant.
Moore Process Controls System Integration & Control Systems Design
Moore Process Controls has successfully modernised a gold processing plant's flotation control system, replacing obsolete I/O hardware with Schneider Electric's latest M580 X80 platform.

Read more...


While every effort has been made to ensure the accuracy of the information contained herein, the publisher and its agents cannot be held responsible for any errors contained, or any loss incurred as a result. Articles published do not necessarily reflect the views of the publishers. The editor reserves the right to alter or cut copy. Articles submitted are deemed to have been cleared for publication. Advertisements and company contact details are published as provided by the advertiser. Technews Publishing (Pty) Ltd cannot be held responsible for the accuracy or veracity of supplied material.


© Technews Publishing (Pty) Ltd | All Rights Reserved