



Abstract
Every year thousands of electrical workers are injured or even killed while at work. To address this issue, safety and trade organisations around the world are enforcing regulations and standards that ensure workers do not open electrical switchgear for maintenance activities unless it is put into a safe work condition, the proper engineering controls and personal protective equipment (PPE) are used and the appropriate level of safety and equipment training is given to everyone involved in the maintenance operation. In the USA and Canada the National Fire Prevention Association (NFPA) and Canadian Standards Association (CSA) are at the vanguard of driving a cultural change within the electrical maintenance industry. The NFPA 70E /70B and CSAZ 462/463 standards and guidelines provide references for facilities to meet the requirements of workplace electrical safety and outline the best practices for setting up and maintaining a safe and efficient electrical preventative maintenance (EPM) programme.
How equipment fails
When deciding on an electrical maintenance strategy we first need an understanding on how equipment fails. A valuable resource can be found by reviewing the failure patterns detailed in the Reliability Centred Maintenance (RCM) engineering framework (see Figure 1). These patterns seem to go against common perceptions that age-related failures account for most of the failures that we see in the field; in fact, it is quite the opposite. This type of failure only accounts for 11% of all the failures that we see.
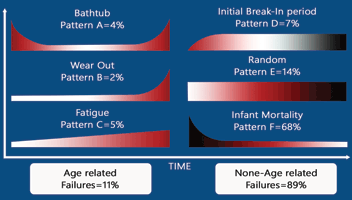
When we look at the curves in Figure 1 we can see how important it is to try to identify failures as early as possible. To allow us to do this we need to understand how failures occur and how these failures affect the function of the equipment. To help with this we use a P-F Curve which is a curve that represents how equipment fails and how early detection can assist in allowing an organisation to plan repairs and avoid business disruption.
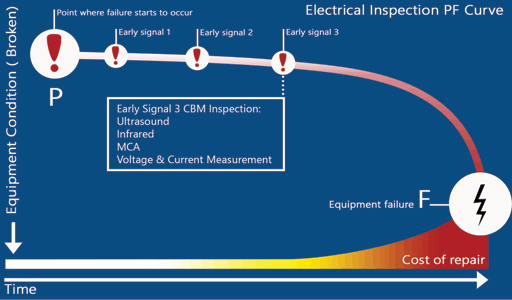
Figure 2 shows an electrical inspection P-F Curve. Point P on the curve is where a physical failure starts to occur which is an identifiable physical condition that indicates a functional failure is imminent. Point F on the curve is the point where functional failure occurs, which is the inability of the equipment, or the assembly containing it, to meet a specified performance standard. An electrical system failing to supply power would be considered a functional failure.
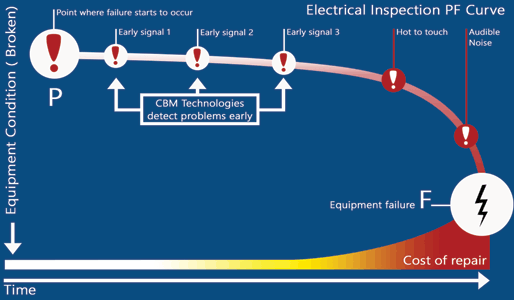
We use Condition Based Maintenance (CBM) equipment to identify the presence of a failure mode, this then allows us to plan and schedule the work early enough before a total functional failure occurs. Figure 2 shows three stages of early detection at which point the CBM equipment test results would be different and the equipment readings would change depending on the severity of the faults being monitored.
It is recommended that a thorough assessment of the equipment and systems that you wish to inspect is conducted before starting a CBM programme. RCM practices give an operator several steps that should be considered while conducting the equipment assessment, these are:
• Functions: Clearly describe main and support functions as well as performance standards we need to maintain.
• Functional failures: Describe the inability to maintain specified performance standards.
• Failure modes: The specific manner or sequence of events that result in functional failure. (What caused the component to fail?)
• Failure effects: What happens when each failure mode occurs? Events that lead to failure.
• Failure consequences: How does the failure impact your business? (Hidden, EHS, operational, non-operational.)
• Develop maintenance task: What tasks are best suited to mitigate the failure mode?
• Reduce consequences: What can be done to reduce the consequences of failures where there is no scheduled maintenance task? (Consequence reduction tasks)
Conducting an RCM analysis will enable you to predetermine the types of inspection that need to be completed as well as the inspection alarm criteria and the actions that will need to be taken should these be breached. This will save a lot of time, stress and effort if the equipment starts to fail because you would have already decided on the course of action that will be taken which allows for much greater efficiencies in the maintenance and repair process.
Unfortunately it is recommended that all CBM tasks be completed while the equipment is energised, in normal operating mode and under load (this is what NFPA 70B and CSA Z463 recommend). As the essential element for electrical safety is to ensure that the equipment is in an electrically safe condition before any work is commenced, keeping personnel away from energised electrical equipment is paramount. At the core of all safety initiatives is the hierarchy of control. Put simply, this concept attempts to control or mitigate risk wherever possible. In order of preference, the hierarchy of control seeks to mitigate risks by:
1. Risk elimination.
2. Substitution (with lower risk).
3. Engineering controls (such as arc resistant switchgear).
4. Safe work practices.
5. Personal protective equipment (PPE).
Before conducting any maintenance task you must ensure that, if possible, you eliminate any risks to the maintenance engineers or operators – PPE should always be the last line of defence. This is why many companies are adopting the use of several types of electrical maintenance safety devices (EMSDs) to include thermal imaging equipment, infrared (IR) windows; ultrasound guns, ultrasound ports, on-line monitoring systems, etc. EMSDs allow CBM inspections to be completed while the switchgear remains closed and in a safe and guarded condition ensuring inspectors are never exposed to the dangers of arc flash or electrocution during the inspection process.
The benefit of using EMSDs is that they standardise the inspection routes by becoming data collection points for the CBM test equipment, they also ensure all inspection parameters are fixed and that all data collection practices are standardised, ensuring that trend analysis data is accurate and repeatable. Other benefits include:
• Switchgear is maintained in a closed and guarded condition.
• Remove risk of electrocution and possible triggers of an arc flash incident.
• Removal of high risk behaviours.
• Conduct fully-loaded, on-line inspections (when they are the most valuable).
• Access inaccessible equipment.
Because there is no panel removal required:
• Inspections require less manpower.
• Inspections require lower PPE levels.
• Inspections are faster and more efficient.
• More inspections are completed due to ease of operation.
Types of EMSD
Infrared (IR) inspection windows
One of the tasks that need to be completed on electrical equipment while it is energised and under load is infrared (IR) scanning. IR cameras can only measure what they can see (direct line-of-sight) and cannot see through glass or plastic viewing windows commonly fitted in switchgear. To allow the inspections to be completed under load we use an IR window which is an EMSD that allows an IR camera to see the energised loaded connections through a special lens material in the IR windows while the switchgear remains closed and in a safe and guarded condition.
Airborne ultrasound ports
Ultrasound equipment can be used to detect arcing, tracking and corona in electrical equipment. To allow these inspections to be made the ultrasound equipment requires access to the energised electrical equipment. This type of equipment can utilise ventilation grills and door seams to access the majority of equipment but requires ultrasound ports to be fitted to environmentally sealed units (NEMA 4/IP65 and above) to allow access to the energised equipment. Ultrasound inspection ports should be IP2X compliant and contain an internal grill for additional security. We see ultrasound ports being used more and more in all types of electrical switchgear as a standard collection point for ultrasound data.
External voltage and current measurement ports
Voltage and current measurement of electrical equipment is essential as it gives us an indication of the system’s overall efficiencies and very small variations in these measurements can show the onset of significant faults. We use external voltage and data ports to allow operators to get the data they require without having to open the energised panels and touch conductors with test equipment such as power quality meters, MCA testers, voltmeters, etc.
Discussion of the results and benefits of early detection using EMSDs
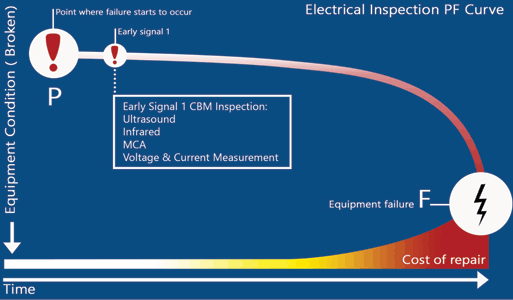
Early signal 1
This is the point immediately after failure starts to occur. The signs at this stage are quite subtle but should show a marked change from the benchmark data from previous inspections especially on the voltage/current, infrared and ultrasound measurements. Usually results in increased inspections of the suspect equipment to track changes.
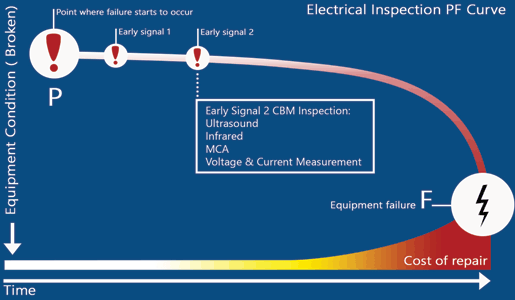
Early signal 2
This stage shows an increase in the previous voltage/current and ultrasound measurements taken at stage 1 and the IR inspections would start to show significant heating at the faulty joint/components. This is normally where the shutdown and repair work would be booked and scheduled as well as any faulty replacement components ordered. Inspections would continue to be conducted to ensure the faulty joint/component does not degrade where it could affect safety/operational requirements.
Early signal 3
This stage is where all CBM readings have reached critical limits where an immediate shutdown would be required or extreme operational changes implemented to allow for the repair to be scheduled such as load reduction on equipment, partial shutdowns, etc.
Final stages of electrical failure
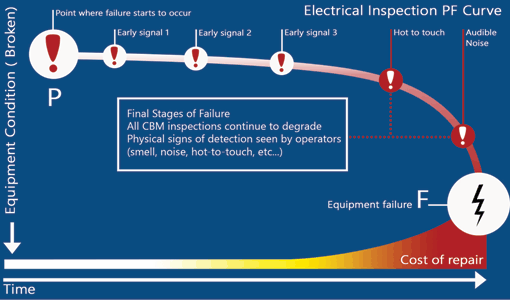
Final stages of failure are evident even without using CBM test equipment. At this stage operators will be reporting the physical signs of failure such as noise, smell of burning, hot to touch, etc. These signs normally precede the point where a functional failure occurs and at this stage the cost of repair is usually much higher than it would have been if the repairs were completed at the first signs of failure.
Summary and conclusions
Online monitoring using EMSDs bridges the gap between annual CBM inspections by monitoring and reporting critical parameters within electrical enclosures on a daily basis. If a critical issue arises, immediate notification allows for an appropriate corrective action, before costly damage occurs. The system alarms allow for maintenance technicians to be warned of potential issues causing the elevated internal ambient temperatures. This information and trend data gives maintenance personnel an enormous safety advantage compared to any type of routine maintenance or troubleshooting of possible electrical anomalies within the electrical enclosures.
The implementation of online monitoring and closed loop EMSD solutions for electrical distribution systems give engineers a solid foundation to build a safe and effective electrical preventative maintenance programme and show reductions in equipment failure and maintenance costs due to early fault diagnosis. This methodology ensures that if conditions are ever met where equipment will possibly fail the equipment shut down and repair can be planned well in advance, replacement parts are ordered and labour resources allocated ensuring that there is minimum disruption caused to the operation.
Equipment maintenance is dictated by actual, real-time reports of equipment degradation rather than by equipment legacy reports. Equipment maintenance practices change from a mainly reactionary/part preventative activity to a mainly preventative/part reactionary activity that enables maintenance engineers to focus their time and resources where they are most needed. Readers wanting to review a previous article on the subject can visit: http://www.instrumentation.co.za/51163n
| Tel: | +27 11 608 1551 |
| Email: | [email protected] |
| www: | www.randci.co.za |
| Articles: | More information and articles about R&C Instrumentation |






© Technews Publishing (Pty) Ltd | All Rights Reserved
 printer friendly version