



Mining is a hazardous environment at the best of times and is becoming increasingly complex, with long-distance conveyor systems, underground networks and distributed electrical infrastructure all posing increasing safety challenges. As sites expand, systems must transmit shutdown commands reliably over tens of kilometres and verify that they have been executed. Ian Loudon, international sales and marketing manager at remote monitoring specialist, Omniflex highlights the importance of fibre optic technology in delivering this.
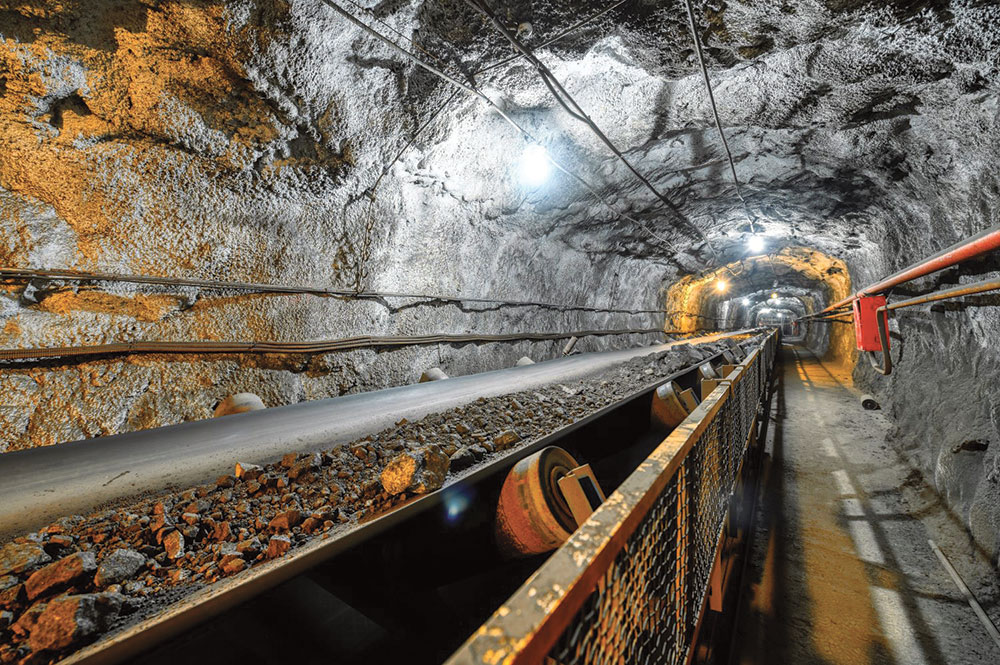
Conveyors are the backbone of coal extraction, transportation and processing, but they also represent one of the greatest sources of operational and safety risk. As mines have grown larger and more complex, belts that once stretched a few hundred metres now extend for many kilometres, often across uneven terrain or deep underground. Ensuring safe operation across these vast distances depends on reliable emergency signalling, responsive shutdown systems and verifiable feedback loops.
Conveyor belts often run up to 20 to 30 kilometres with multiple drive motors, synchronised PLCs, and intermediate loading or discharge points. When failure occurs at any point along that distance, the consequences can escalate rapidly.
Traditional copper cabling was never designed to carry safety-critical signals over the 10 to 30 kilometre spans now common in mining operations. Signal degradation, voltage drop and electromagnetic interference (EMI) from surrounding drives, motors or switching equipment all undermine reliability. When signalling runs require repeaters, the number of dependency points increases and so does the potential for failure.
Copper cabling is therefore no longer fit for purpose in long-distance or electrically hostile mining environments. Lengthy copper runs are prone to EMI and voltage loss, while any attempt to push signals beyond around 10 kilometres typically demands additional converters or amplifiers, creating further vulnerability. Underground, signal strength can also be limited as dense rock formations and heavy electrical infrastructure disrupt transmissions.
Most importantly, traditional one-way signalling introduces dangerous uncertainty. In the event of a shutdown request, mines are left relying solely on the fact that a command was sent, rather than knowing that it was received and acted upon. For safety-critical equipment such as conveyors, crushers or ventilation systems, certainty is everything.
How fibre optic technology provides certainty
To address the reliability limits of copper and legacy one-direction shutdown circuits, many operators are now turning to fibre optic transmission for safety-critical signalling. Fibre offers several advantages in mining environments. It is immune to EMI, intrinsically non-sparking and capable of reliably transmitting contact signals over distances of 20 to 30 kilometres. In long-distance conveyor networks, deep underground haulage routes or electrically hostile substation areas, these characteristics eliminate many of the vulnerabilities that compromise the performance of conventional systems.
The most important evolution in thinking is the shift from simply issuing a shutdown signal to verifying its result. In mining environments, the difference between ‘signal sent’ and ‘shutdown confirmed’ can determine whether machinery continues running with a damaged belt, a stalled crusher or elevated gas readings.
Specialist fibre optic modules designed for safety-critical applications, including SIL-rated bi-directional contact repeaters, embody this approach. These devices replicate contact states over long distances while providing dual-redundant monitoring and clear feedback to the originator. By transmitting both the initiating signal and its confirmation across the same optical link, they reduce uncertainty, minimise wiring infrastructure and support compliance with mine shutdown, emergency isolation and interlock requirements.
As conveyor systems grow longer, underground workings expand and electrical networks become more distributed, this approach offers a path to greater resilience and clarity. Rather than relying on inferred responses, operators benefit from definitive proof that the shutdown command travelled, the machinery responded and the system is now in a safe state. That level of certainty forms the basis of a robust safety culture within modern coal operations, reflecting a broader industry shift toward verified safety rather than assumed outcomes.
Omniflex has extensive experience in engineering SIL-rated fibre optic systems for long-distance, safety-critical environments. Our fibre modules are designed for bi-directional contact replication, auxiliary confirmation and failsafe behaviour, and have been deployed across mining, nuclear and electrical infrastructure where reliability and verification are paramount.
| Tel: | +27 31 207 7466 |
| Email: | [email protected] |
| www: | www.omniflex.com |
| Articles: | More information and articles about Omniflex Remote Monitoring Specialists |






© Technews Publishing (Pty) Ltd | All Rights Reserved
 printer friendly version