



Members of a certain generation may remember that their first PLC was equipped with no more than 8 kB of memory.
Thanks for the memory
Today it is not unusual to see even base-line systems offered with memory capacities and supported network protocols that make those early systems pale into insignificance.
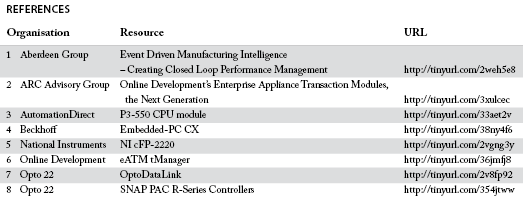
Examples include AutomationDirect’s recently introduced Productivity 3000 controller3, National Instruments’ NI cFP-2120 Compact Real-Time Controller5 and Opto 22’s SNAP PAC R-Series Controllers8. The former is fitted with 50 MB total available user memory for application data and documentation storage and has built-in support for Modbus TCP Client and Server (Ethernet). The NI unit offers 256 MB DRAM , 256 MB non-volatile storage, removable CompactFlash and USB storage and two 10/100BASE-T Ethernet ports with embedded Web and file servers and remote-panel user interface. Opto 22’s SNAP PAC R-Series Controllers offer up to 4 MB of memory for PAC Control Strategy, 2 MB for local file storage and up to 2 GB of removable storage via MicroSD card. Installing the OptoDataLink software7 on such a controller opens the path to enterprise databases including MS SQL Server and MySQL.
While some vendors have stuck with proprietary hardware solutions and steered clear of PC technology at the factory floor, vendors like Beckhoff have worked at offering hardened PC-based technology. Beckhoff’s Embedded-PC CX can withstand the process environment and support real-time kernels working in tandem with commercial off-the-shelf operating systems. The CX5000 series has 512 MB RAM, a 64 MB CompactFlash card and two RJ45, 10/100/1000 Mbit/s Ethernet ports.
In between these two approaches are products from niche vendors like Online Development who have developed back-plane modules that can be used with Rockwell controllers and standalone panel mounting modules that work with Rockwell, Schneider and Siemens controllers. These robust Appliance Transaction Modules6 (ATMs) provide tightly integrated, secure, user-configurable data transfer with store and forward buffering to many databases including MS SQL Server, MySQL, Oracle and IBM along with support for messaging queues like Java Messaging Service (JMS).
Downward spiral
These developments have paved the way for the downward migration of fault-tolerant file I/O from traditional ISA-95 level 3 and above. And this has opened up a plethora of real-time and near real-time control opportunities. Advanced Process Control, data-logging and process control techniques like statistical process control (SPC), which are reliant on database capabilities, can now happily reside on the factory floor or directly influence manufacturing operations without the need for scada software modules as a bridge between controllers and databases.
At the same time the technology built in to the software and/or hardware connectivity tools has removed the need for bespoke programmed solutions for database links. Connecting factory floor data directly to manufacturing and enterprise databases is now as simple as populating a form to create links between control system I/O points and/or local variables on the one side and database points on the other.
User benefits
An Aberdeen Group report1 on event driven manufacturing intelligence identified reducing variability in product processes as a key action in reducing manufacturing costs. The research revealed that best-in-class organisations were more than four times as likely to display operational data and metrics in real-time and named SPC as one of the enablers for reducing manufacturing costs.
According to ARC Advisory Group2, “The growth of Automation Appliances has been fuelled by their inherent benefits that include ease of use, low installation costs, reliability, flexibility, data security, and scalability. These benefits make Automation Appliances a practical choice to support a variety of applications such as downloading batch recipes and process line configuration, tracking and tracing, build orders and inventory management, dynamic palletizing and delivery route instructions, and integrating workflow with business processes. By using Automation Appliances to convert manual tasks into automated systems, end users can achieve faster product changeovers, better equipment utilisation, higher quality levels and production rates, increased response to customer orders, and lower labour rates.”
There are real benefits to be gained by leveraging IT technologies at the plant floor.
Real-time SPC
The GainSeeker Suite from Hertzler Systems is an example of a real-time SPC offering. This comprehensive SPC package includes an OPC interface for connection to real-time systems. The OPC capabilities of the product suite were demonstrated at the OPC Foundation’s Interoperability Workshop 2010 in May. In addition to OPC communications the software has drivers for many well-known electronic weigh scales, digital gauges, vision equipment and inspection equipment.
Application example – SPC
In a packaging/filling operation, net weight control is a crucial component in maximising profitability. Underfilling may result in fines and customer loss; overfilling means giving product away. In the USA weight controls should meet the requirements of NIST Handbook 133 and various regulatory bodies. Typically these regulate minimum mass but place no limits on maximum mass. In order to meet the minimum requirements, filling machines are often set so that the mass at the thin tail of the minimum meets the standard. Consequently average mass is above declared mass.
McCormick Flavor Division, a division of McCormick & Company, has successfully applied the GainSeeker SPC suite with automated data collection. By gaining insight into the variability in its processes the division has been able to reduce overfill by 0,3 g per pack across all its filling lines, saving significant amounts of money. It has also achieved major savings in its premix operations through the application this technology.
Application example – OptoDataLink
NASA’s Deep-Space Network (DSN) is responsible for collecting data from satellites and space probes. This is achieved through three deep space communications facilities located in California’s Mojave Desert; near Madrid, Spain; and near Canberra, Australia.
The Jet Propulsion Laboratory (JPL), under the auspices of the California Institute of Technology, manages the DSN antennas for NASA. Fault-free operation is essential as there are no second chances to obtain data that is coming in from space probes that are travelling at up to 50 000 km/h. The moving parts of the larger antennae weigh nearly 2000 tonnes and during an inspection cracks were found in the elevation bearings.
To study the causes of these failures special plates equipped with load cells have been fitted to the dish support mechanism. The signals from these load cells have been connected to analog inputs on distributed Opto 22 SNAP-PAC-EB2 controllers which are networked via Ethernet to a SNAP-PAC-R2 controller. From there, data is sent to a JPL database via OptoDataLink, which provides multiple connections for exchanging data between the SNAP PAC System and SQL databases.
Application example – Automation Appliance
To ensure fast and accurate response to customer orders for standard and custom-built trucks, a major manufacturer of heavy-duty trucks used Online Development’s eATM module to pass order data from customer service through a Microsoft SQL database to plant floor part handling systems. These systems are connected via DeviceNet to an Allen-Bradley ControlLogix PAC.
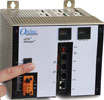
During the assembly process the eATM module queries the database for bill of materials information for truck orders placed by customer service and then interacts with the plant’s inventory handling systems through the backplane of the ControlLogix to stage parts for specific orders on the assembly line.
The module also communicates back to the database to notify customer service that the parts have been assembled, or if any parts are missing that will delay an order. Inventory and production are also kept up-to-date on the status of build orders.
The eATM module’s audit and exception logs let plant personnel, customer service and management know the on-time performance of the entire system. These logs detail all transactions to help plan and implement continuous improvements to the entire system.
About the author
Andrew Ashton has electrical, mechanical and business qualifications and has been active in automation and process control since the early 1980s. Since 1991 he has headed up a company that has developed formulation management systems for the food, pharmaceutical and chemical manufacturing industries and manufacturing solutions involving the integration of various communication technologies and databases. Developed systems address issues around traceability, systems integration, manufacturing efficiency and effectiveness. Andrew is a contributing editor for SA Instrumentation and Control.
| Tel: | +27 11 543 5800 |
| Email: | [email protected] |
| www: | www.technews.co.za |
| Articles: | More information and articles about Technews Publishing |






© Technews Publishing (Pty) Ltd | All Rights Reserved
 printer friendly version