



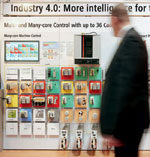
With the company’s C6670 industrial server, Beckhoff has brought to market one of the most powerful, if not the most powerful, machine controller to date, equipped with up to 36 processor cores.
This immense level of performance is harnessed most effectively via TwinCAT 3.1 automation software, exploiting the potential of each individual core to its fullest.
In this interview, managing director, Hans Beckhoff explains the benefits of such many-core machine controllers with regard to current applications and their potential for future innovations.
With its up to 36 processor cores, the C6670 industrial server represents a quantum leap in terms of processing performance for machine control. How did this idea come about?
Hans Beckhoff: Since the CPUs in PCs are among the most powerful processors available today, we offer cutting-edge performance with our PC-based control technology. We continuously push the envelope in automation, based on the advances made in modern processor technology as predicted by Moore’s Law. Current starter processors feature four or eight cores, but processors with up to 64 cores will be considered standard in only a few years. We believe that machine designers should be able to employ a many-core platform already today, either for highly demanding automation tasks or as a visionary operating platform.
What are the benefits of such a visionary operating platform?
Hans Beckhoff: Development towards more and more processor cores will continue unabated. When you have 10 or 20 times more computing performance at your disposal, you can base your machine control technology on a whole new set of innovative concepts. However, since three to five years is not a lot of time to develop a totally new software architecture, the users of automation technology would be well advised to begin this endeavour today. The C6670 industrial server provides the ideal platform to evaluate what a 24-core or 36-core computer can provide for the respective customer application. Machine manufacturers should take advantage of this opportunity since employing such a powerful controller already delivers tangible application benefits for sophisticated automation tasks today.
To what extent are control applications actually suited for such a multi-core architecture?
Hans Beckhoff: Automation technology is the ideal area for multi-core architectures because modern machines comprise a wide range of function modules and many positioning axes. These all operate simultaneously and can be very effectively mapped via individual control programs that run side-by-side. TwinCAT 3 provides optimal support for this approach with its many-core focused features, such as many-core PLC and motion or core isolation, making the parallel control architecture easy to implement. In addition, the high performance EtherCAT communication bus is able to transmit huge data volumes deterministically and with short cycle times. This enables machine builders to test the parallel control architecture on their machine and use the results to develop next generation control technologies.
Which application benefits of the C6670 industrial server can you already implement today?
Hans Beckhoff: We already encounter many highly complex automation applications, such as in wind farm simulations, for example. A single C6670 can reduce the amount of computer hardware required by taking the place of several conventional PCs. This also enables you to replace the data communication between multiple computers with much faster software-to-software communication.
Particularly in machine engineering, we see the tendency to implement many more motion axes, operating them in an ever more dynamic manner and with more complex algorithms. The tremendous performance of the industrial server eliminates many restrictions in machine design. For instance, you can have 200 or more adjustable axes plus integrated measurement functions and condition monitoring feature – all of which falls in line with our concept of Scientific Automation. You can even integrate a vision system – most of which are still running on separate computers these days – into such a centralised computing platform and make image processing more of a standard feature on the machine.
Does this mean that you can develop more powerful machines and systems for all industries?
Hans Beckhoff: Yes, you can, especially in areas where our eXtreme Fast Control (XFC) technology is employed. Many-core control and XFC increase not only the performance of machines and systems – they also improve the product quality with their highly precise and extremely fast control processes, while minimising the consumption of energy and raw materials. In summary, they deliver significant economic advantages as well as sustainability benefits.
Is the C6670 industrial server suited only for centralised control concepts or also for distributed designs?
Hans Beckhoff: The industrial server is mainly a central data processing unit that makes computing, storage and communication capacities available locally. With our modular and scalable control technology, however, we support both concepts as a rule. A large assembly line, for example, is ideal for an automation architecture that features small, distributed controllers. For a packaging or tooling machine with many coordinated movements and conditions, on the other hand, a centralised solution would be the better option. However, our server technology has become so powerful that these distinctions are becoming rather fluid. In concepts with a modular, aggregate-oriented design of controller and machine, the intelligence could be implemented either locally in the individual modules or in a central industrial server using appropriate software modules and fast EtherCAT communication technology.
What about applications with typical server functionalities?
Hans Beckhoff: With its enormous processing performance, the C6670 is also capable of providing true server functions in industrial applications such as those promoted via Industry 4.0. For instance, you might transfer complex mathematical functions to the industrial server in order to enable less powerful controllers to handle the condition monitoring, such as for vibration analysis tasks. This would be a so-called service-based concept, where complex automation services run on a powerful server in order to remove some of the workload from the actual machine controller. If you have a communication bandwidth that is sufficiently fast and deterministic, such a server could even run in the cloud. With the C6670, however, you can provide the necessary performance on-site at the machine or line.
For more information contact Kenneth McPherson, Beckhoff Automation, +27 (0)11 795 2898, [email protected], www.beckhoff.co.za
| Tel: | +27 11 795 2898 |
| Email: | [email protected] |
| www: | www.beckhoff.com |
| Articles: | More information and articles about Beckhoff Automation |






© Technews Publishing (Pty) Ltd | All Rights Reserved
 printer friendly version