


IT in Manufacturing


Pharmacy automation with PC-based control technology

July 2017 IT in Manufacturing

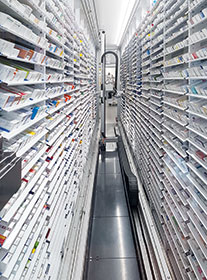
Finnish company NewIcon specialises in automation solutions for pharmacies. The robot-assisted Mega-Fixu storage and retrieval system automates medicine supply and is deployed mostly in hospital pharmacies. The modular solution can be custom-tailored to meet the specific needs of each medical facility. The system can also be integrated seamlessly into the customer’s ERP system, leveraging a Beckhoff industrial PC as the central control platform.

A quick and reliable solution, Mega-Fixu completely automates the identification, shelving and dispensing of medications, enabling pharmacists and medical staff to eliminate tedious and repetitive activities. It also improves safety because the enclosed storage system keeps medications safe and secure and continuously monitors environmental temperature and medication expiration dates. Possible human error when storing and picking medications are therefore a thing of the past. Other benefits include improved workplace ergonomics and more efficient use of space. In terms of scale and cost, each NewIcon storage system is custom-tailored to fit the size and turnover of the respective pharmacy.

High-powered platform integrates PLC, image processing and database functions

The control system and database run on a Beckhoff C6650 Industrial PC (IPC) equipped with a powerful Intel Core i7 quad-core processor as well as a RAID controller and redundant hard disks. The control system, database and ERP link are based on TwinCAT automation software. “The reliability and performance of the IPCs are very important to us because the database comprises 150 000 data points for the various storage positions,” explains Mika Rissanen, automation manager at NewIcon. “In addition, the openness and modularity of the solution were among the criteria that solidified our decision to employ PC-based control technology. The modularity of our system perfectly matches the modular control architecture offered by Beckhoff. We also had the ambitious goal to integrate the database, image processing and automation system on a single PC platform.” The powerful C6650 IPC with EtherCAT as the complete communication system has made this possible. Other system benefits mentioned by Rissanen include lower total cost of ownership and integrated support for remote access. “By implementing a PC-based control system, we now have the option to access Mega-Fixu applications remotely for maintenance purposes,” explains Rissanen.

The Mega-Fixu system has a robot-assisted input unit where each package is identified and measured via a barcode reader and an intelligent image processing system. Following this step, the control system determines the most suitable storage location for the package. The system’s X/Y servo axes controlling the robots that shelve and retrieve medicine packages are equipped with Beckhoff AM8000 series motors that feature One Cable Technology (OCT), as well as 2-channel AX5000 Servo Drives. The servo axes’ movements are controlled via DIN rail-mounted CX5020 Embedded PCs from Beckhoff.

Future developments

“Since the order picking systems for pharmacies and hospitals must work trouble-free and be highly reliable, it’s best when service and maintenance are performed proactively,” explains Rissanen. “The number of systems we have shipped has increased so rapidly that we are considering an even more comprehensive diagnostic and monitoring approach. The TwinCAT IoT and TwinCAT Analytics software tools will make it easy for us to integrate cloud-based services and automated diagnostics into our systems in the future,” says Rissanen. “We appreciate that Beckhoff provides the ability to use the Internet of Things as an integrated part of an automation system and also as a simple, totally separate data collection system that can even be added to existing installations.”

For more information contact Kenneth McPherson, Beckhoff Automation, +27 (0)11 795 2898, [email protected], www.beckhoff.co.za


Credit(s)


Share this article:
Share via emailShare via LinkedInPrint this page

Further reading:

Even in autonomous systems, human insight is important
Schneider Electric South Africa IT in Manufacturing
As AI, IIoT and digital twins reshape industrial operations, Schneider Electric’s Kobus Vermeulen and Bafana Msibi argue that the operator’s role is shifting from controlling equipment to interpreting intelligence, validating AI recommendations and making decisions that improve

Read more...
AI-based quality inspection scales across P&G operations
Siemens South Africa IT in Manufacturing
Siemens and Procter & Gamble are expanding an AI-based visual inspection system across P&G’s manufacturing operations worldwide, inspecting products in real time at full line speed, and reducing scrap rates by 10 to 20% depending on the product.

Read more...
How sustainability unlocks real business impact
Rockwell Automation IT in Manufacturing
Sustainability has moved from a compliance obligation to a strategic driver of resilience and value for manufacturers. Rockwell Automation explains how its Triple A framework and connected-data approach help producers cut energy, water and waste while improving productivity.

Read more...
Mining’s AI future will depend on people as well as technology
IT in Manufacturing
South Africa’s mining industry is embracing digitalisation and AI, but AvenirHoldings chief executive officer, Tshidi Mndzebele says the real test is whether the people behind the industry are equipped to move forward with it, and outlines five things mining needs to get right.

Read more...
How BIC overcame operational silos to integrate technology and people
Rockwell Automation IT in Manufacturing
Manufacturing giant BIC deployed Plex MES from Rockwell Automation at its Bizerte plant in Tunisia, replacing fragmented, partly in-house software with a single cloud-based execution system that broke operational silos and improved shop-floor visibility.

Read more...
AI in industry is an early warning system, not a guarantee
Schneider Electric South Africa IT in Manufacturing
Schneider Electric’s Paul Steyn argues that AI in industrial maintenance is only as good as the infrastructure and people behind it, and explains the three layers a facility needs before predictive maintenance can deliver on its promise.

Read more...
SA’s mining industry must put people at the heart of its digital future
IT in Manufacturing
South Africa’s mining industry employs around 470 000 people while its digital transition accelerates. Avenir’s chief executive officer, Tshidi Mndzebele argues that technology should enable and upskill the workforce rather than replace it, setting out five ways mining can make technology work for its people.

Read more...
Quality control supports efficient tissue production
Valmet South Africa IT in Manufacturing
Valmet’s advanced quality control technology is helping tissue producers improve product consistency while reducing energy and raw material consumption. Its latest installation at KORO Paper in Vietnam combines real-time measurement, process optimisation and non-contact, nuclear-free quality control.

Read more...
Patented algorithm maximises operator efficiency
Rockwell Automation IT in Manufacturing
Rockwell Automation piloted a patented anomaly detection algorithm and FactoryTalk DataMosaix at its Twinsburg electronics plant, giving operators 30 to 60 days’ advance warning of stencil failure, improving fail rates by 22% and achieving a 200% return on investment.

Read more...
Cybersecurity must become part of the next era of industrial automation
Adroit Technologies IT in Manufacturing
The EU’s Cyber Resilience Act is setting a global benchmark for connected products, making cybersecurity a core engineering requirement in industrial automation. Adroit Technologies and Mitsubishi Electric explain how building security into controllers, PLCs and drives from the outset helps South African manufacturers protect production and meet international expectations.

Read more...


While every effort has been made to ensure the accuracy of the information contained herein, the publisher and its agents cannot be held responsible for any errors contained, or any loss incurred as a result. Articles published do not necessarily reflect the views of the publishers. The editor reserves the right to alter or cut copy. Articles submitted are deemed to have been cleared for publication. Advertisements and company contact details are published as provided by the advertiser. Technews Publishing (Pty) Ltd cannot be held responsible for the accuracy or veracity of supplied material.


© Technews Publishing (Pty) Ltd | All Rights Reserved

