
Artificial intelligence (AI) has hit the headlines recently, with a great deal of media coverage dedicated to how ChatGPT and similar technologies are making their mark on our everyday lives. With all this attention, you could be forgiven for thinking that AI is a new technology. In fact, AI can date its origins back to the 1950s. What we are actually seeing today are the results of decades of research and technological developments; they just all seem to be coming to mainstream fruition now, making a real difference to how we live and work.
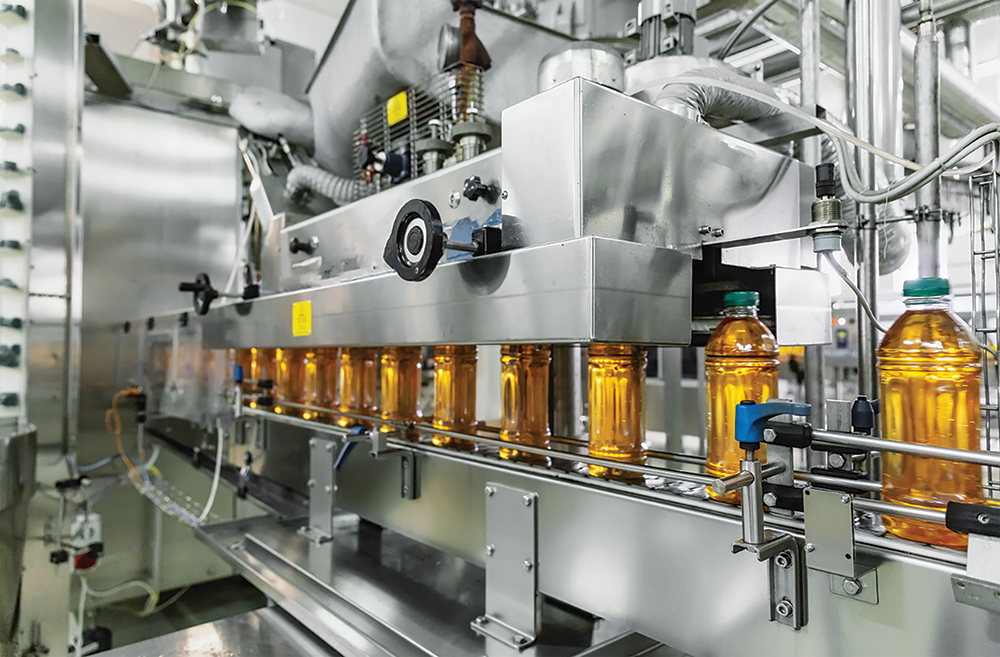
When it comes to the food and beverage sector, things are no different, and more businesses are reaping the benefits of AI technologies. With the value of the market for AI in the food and beverage sector expected to reach a staggering $30 billion by 2028, the number of food and beverage businesses investing in AI is clearly predicted to increase. But while many in the industry have heard of AI, there is still widespread uncertainty about what it actually is, how it works and how it can benefit the food and beverage sector.
What is AI? What is machine learning (ML)?
AI is the ability of a computer or machine to mimic or imitate human intelligent behaviour and perform human-like tasks. It performs tasks that require human intelligence such as thinking, reasoning, learning from experience, and making its own decisions. ML is a subset of AI. It involves computer systems that can learn and adapt without being explicitly programmed or helped. ML uses algorithms and statistical models to analyse data intelligently, drawing inferences from data patterns to inform further action.
Where does AI fit into the food and beverage sector?
AI has the potential to optimise all areas of food manufacturing. It can facilitate smart, industry-specific applications to improve every aspect of the supply chain from farm to fork, helping to build agile supply chains and drive revenue growth. With its ability to factor in an inordinate number of data values, parameters, what-if scenarios and other contributing factors, ML can produce accurate and timely recommendations for almost every aspect of the food supply chain. Ultimately, this provides a competitive advantage that would be impossible to replicate without the application of AI technologies.
Where is ML being used already?
The uses of ML for the food and beverage sector are seemingly limitless. Take precision farming for example, an area where it is delivering new depths of insight. An example is the analysis of past harvests in terms of both quantity and quality, in combination with weather forecasts to inform which fields need watering and when to use fertiliser.
In the aquaculture sector leading animal nutrition company, Nutreco has achieved additional production cycles and healthier shrimps, while at the same time using 30% less feed. The business uses audio sensors in aquaculture to ‘listen’ to the shrimps, understanding when they are hungry. ML then determines when and how much the shrimps must be fed, which lowers the feed conversion ratio and shortens the shrimp production cycle, doubling production without huge intensification.
Another example of ML in action is at a global bakery ingredients business, Zeelandia. The business has addressed the challenges of higher costs and lack of available bakery ingredients by deploying an ML model that recommends products and prices to be offered to their bakery customers based on what similar customers are buying. Through the implementation of applied AI, the group has achieved an 83% faster time to prepare product recommendations for customers, cutting the time down from 30 minutes to five minutes. As a result of product recommendations taking less time, Zeelandia employees are able to provide a better customer experience. In addition to increased revenue per transaction and share of wallet per customer, the company is improving the accuracy and speed of product recommendations and pricing strategies.
We are seeing more food and beverage organisations turning towards AI to help reduce waste and identify inefficiencies within the supply chain. Leading global provider of goat and organic cow cheese, Amalthea, is using ML to make the cheese quality more predictable and to maximise yield, building customer loyalty and boosting sustainability. Previously Amalthea could only manually analyse milk yield on a weekly basis, which made it difficult to adjust the process parameters to optimise the yield. By leaning on ML, Amalthea can now view the yields immediately, in addition to receiving direct insight into what is causing a yield change. This has helped Amalthea to reduce its overall waste from manufacturing, as the company can quickly identify pain points and improve processes simultaneously. These changes have had a direct impact on the company’s profitability and bottom line. For every 1% increase in yield, Amalthea expects to save approximately €500 000.
Planning for all eventualities
Nowadays, food businesses could be forgiven for thinking that the only thing that they can be certain of is uncertainty itself. With more unpredictable variations in weather conditions, what about the role of ML where there are potentially no data patterns to be found? What ML can do is help understand the risks of changing weather conditions better, and how they can impact harvests globally. It is this increased understanding that can inform the strategies needed to mitigate these risks. But ensuring these strategies are effective requires consensus. As the UN’s Food and Agriculture Organisation (FAO) points out, every party involved in the food supply chain needs to become more resilient, minimising the use of water, energy and other resources. These are all changes that can be underpinned by ML.
As technology develops and as more businesses discover the benefits that can be realised with the application of AI, so AI capabilities will develop further, and be refined to solve specific industry or business problems. As we are seeing already, the considered application of AI technologies is helping businesses right across the food and beverage industry supply chain, and this is set to increase over the next few years. AI is already proving to be a driver of real efficiencies, and is helping businesses to plan for all eventualities, delivering the actionable insight needed to stay a step ahead at all times.




© Technews Publishing (Pty) Ltd | All Rights Reserved
 printer friendly version