Case history 186: Don’t always trust valve position feedback signals
March 2023
Editor's Choice
PLCs, DCSs & Controllers
I recently encountered an interesting problem in a minerals recovery processing plant. The loop in question was a gas flow control to a burner and was considered very important for the process temperature control. The operators reported that the loop cycled badly in automatic, and was very difficult to control manually. The C&I technicians had tried all sorts of tunings without any improvement.
They included this loop in a series of optimisation tests we were doing as part of the practical we held after they had finished the classroom part of my basic control course. They said they knew that valve problems often cause problems for control but that this loop had a valve position feedback signal on it and the feedback signal closely followed the controller output signal so they were pretty sure it wasn’t the cause of the problem.
The first test we normally carry out is a Closed Loop As Found test and we recorded how the loop responded to setpoint (SP) changes in automatic with the original existing tuning parameters. However, as reported, the loop cycled badly.
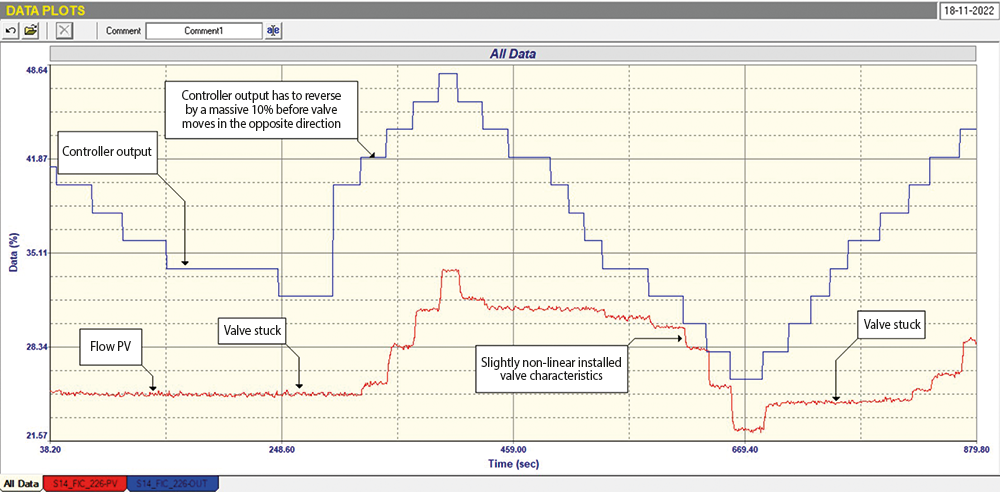
The second test was an Open Loop test where the controller is placed in manual, and various steps are then made on the PD (controller output). Part of this test is shown in Figure 1. Unfortunately we did not record the valve position feedback signal. It can be immediately seen that there was in fact a huge valve problem as the valve was not only apparently sticking in places but also had huge ‘almost hysteresis’ of over 10%. I say ‘almost hysteresis’ because it did move a little on most reversals and then stuck whilst the PD had to move a further 10% before the valve moved again. This was the major reason for the cycling.
Figure 1. Open Loop test
The question is why the valve feedback signal followed the PD so closely. The answer is, and this is something every control practitioner should be aware of, valve position feedback signals generally do not track the actual valve position, but track the position of the actuator. Now depending on the type of valve and actuator, there are often various linkages joining the two. In this case the valve was a butterfly valve, which is a rotary valve. The actuator was a spring and diaphragm type which has a linear action. To convert the linear action to a rotary action, manufacturers employ various techniques, typically geartrains. Therefore the hysteresis and/or apparent stickiness may actually be due to play in the linkages.
On the steps where the valve, and hence the flow PV, did follow the PD, we were able to see that there was a slight non-linear installed characteristic in the valve, and we were able to establish the process dynamics to allow us to get good tuning parameters. The original tuning parameters were actually too fast and were contributing to the cycling, so it was not only due to the valve problem, and the tuning was also causing instability.
Figure 2. Final Closed Loop test
Final Closed Loop test with the new parameters is shown in Figure 2 and is interesting. On the SP step down it can be seen how the valve started moving and then stuck, and the PD then integrated down well over 10% before the valve could move again and bring the PV back to SP. On the SP step up the valve initially didn’t move at all until the PD had integrated up the same amount, and then it moved to get the PV to SP.
This is another example of how important it is to analyse a loop before tuning and to be aware of the various problems that can exist. As I have said many times in the past, the old adage that tuning can solve all problems is nonsense. I have seen the same problem of slippage in the valve linkages many times in the past, and it somis ething that not many C&I; practitioners seem to be aware of.
About Michael Brown

Michael Brown.
Michael Brown is a specialist in control loop optimisation, with many years of experience in process control instrumentation. His main activities are consulting and teaching practical control loop analysis and optimisation. He now presents courses and performs optimisation over the internet.
His work has taken him to plants all over South Africa and also to other countries. He can be contacted at: Michael Brown Control Engineering CC, +27 82 440 7790
Further reading:
SEW-EURODRIVE’s expanded local engineering capability
SEW-EURODRIVE
Editor's Choice Motion Control & Drives
At Electra Mining Africa, SEW-EURODRIVE demonstrated how its expanded local engineering capability, digital technologies and lifecycle support strategy help customers improve reliability, energy efficiency and total cost of ownership across the full life of their drive assets.
Read more...
Calcamite partners with Schneider Electric and 4Sight for smart water management
Schneider Electric South Africa
Editor's Choice
Schneider Electric, AVEVA and 4Sight OT Automation are helping South African wastewater specialist, Calcamite, digitalise its modular treatment plants through a scalable edge-to-cloud automation platform, with the award-winning Gourikwa pilot now scaling to hundreds of remote sites.
Read more...
Paper might carry the message but pressure carries the process
VEGA Controls SA
Editor's Choice
Accurate pressure measurement is critical throughout pulp and paper production, from chemical pulping to steam drying and wastewater treatment. VEGA’s VEGABAR transmitter range offers South African mills robust, precise monitoring for these demanding conditions.
Read more...
BMG integrates conveyor drive technology to improve mining reliability and availability
Bearing Man Group t/a BMG
Editor's Choice
BMG supplies engineered turnkey drive packages for belt conveyors and feeders in mining and bulk materials handling, bringing the motor, drive, couplings, gearbox, lubrication and condition monitoring together as one integrated system to protect conveyor availability.
Read more...
Economy drive system closes the drive gap in the entry-level segment
Beckhoff Automation
Editor's Choice Motion Control & Drives
Beckhoff has launched an economy drive system pairing its new AX1000 servo drive and AM1000 servomotor with the AF1000 dual-axis variable frequency drive on a shared EtherCAT platform, targeting series machines and price-sensitive markets without sacrificing TwinCAT integration or functional safety.
Read more...
South Africa’s space balls
Editor's Choice News
South African engineers are preparing to take low-frequency radio astronomy to the Moon with three locally developed B.A.L.L.S. spheres aboard China’s Chang’e-8 mission. This could pave the way for a 55-antenna lunar array and marks another step in the country’s growing space engineering capability.
Read more...
Practical tips to build a successful engineering career
Editor's Choice
Award-winning civil engineer, Tinashe Mukalela of AvenirHoldings shares ten practical tips for young engineers navigating a competitive job market, from professional registration and mentorship to emotional intelligence and leadership development.
Read more...
Why mining operations need local lightning early warning
Senseca
Editor's Choice Electrical Power & Protection
Lightning can develop into a serious mining hazard before the first local strike, leaving crews little time to stop work and reach safety. Local early-warning technology can provide valuable lead time, allowing mines to connect developing storm conditions to defined trigger actions that protect people, explosives and equipment.
Read more...
XPlanar aids innovation in laser processing
Beckhoff Automation
Editor's Choice Motion Control & Drives
Aalborg University is among the first in the world to test Beckhoff’s XPlanar intelligent transport system in advanced laser processes, achieving micrometer-precise workpiece positioning and dramatically shorter lead times compared with traditional tool-based manufacturing.
Read more...
The wireless route to safer, more efficient mining operations
Emerson Automation Solutions
Editor's Choice Sensors & Transducers
Modern wireless level measurement technologies are helping mining operations improve process control, increase safety and reduce installation costs. Emerson’s Rosemount 3408 wireless non-contacting radar level transmitter uses 80 GHz frequency-modulated continuous wave radar with HART communication to reach remote assets where cabling is impractical.
Read more...




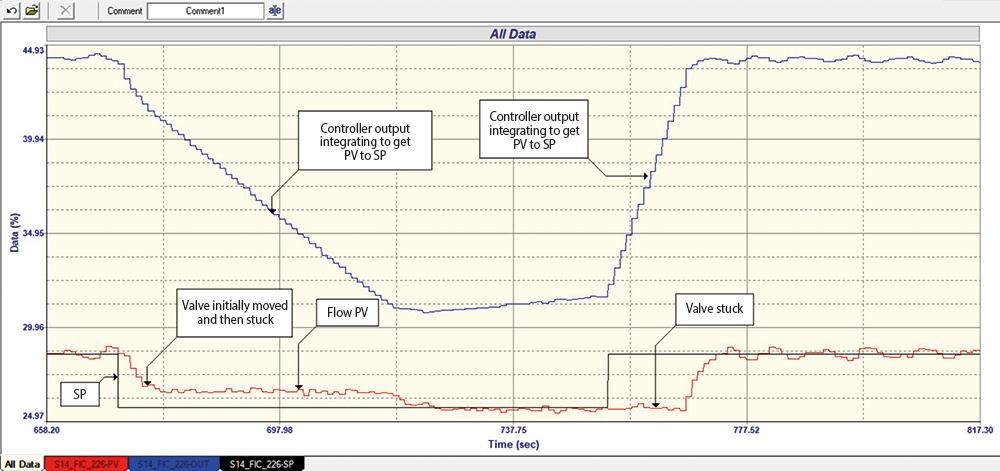 Figure 2. Final Closed Loop test






 printer friendly version