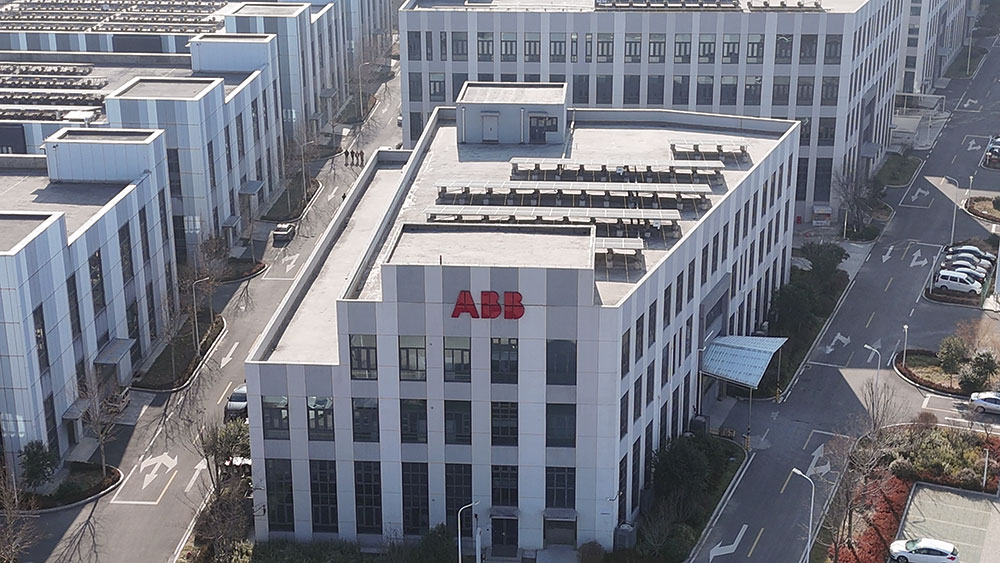
ABB’s production facility in Zibo, Shandong province, China is delivering measurable energy and emissions reductions through the implementation of advanced digital energy management and electrification solutions. Driven by a site-wide sustainability roadmap focused on energy efficiency, electrification, renewable electricity and digital energy management, the site has cut energy consumption by 71 MWh and avoided over 63 tons of CO2 emissions annually, the equivalent to the electricity needed to power several hundred average homes for a month.
The facility has implemented a range of efficiency upgrades across core operations. LED lighting has been installed, air conditioning systems have been optimised based on real-time occupancy data, and upgrades to air compressor controls have reduced unnecessary energy use. Together, these initiatives are improving operational efficiency while lowering both emissions and costs, demonstrating how digitalisation and smart energy management can accelerate low-carbon manufacturing.
The Zibo site, which manufactures wiring accessories for the company’s smart buildings portfolio, has installed an ABB energy management system that monitors, analyses and optimises energy performance across the site. This platform provides real-time visibility into energy consumption, enabling continuous improvement and data-driven decision making.
Building on these efficiency gains, the manufacturing facility operates entirely on renewable electricity, with approximately 15% of the site’s electricity demand now covered through renewable electricity generated by rooftop photovoltaic panels installed within the industrial park, complemented by certified green electricity procurement. The site is certified to ISO 50001 for energy management and has been recognised by local authorities as a Zibo City-level Green Factory, highlighting its role as a regional benchmark for sustainable industrial operations.
“The progress at Zibo shows how Mission to Zero is translated into measurable results,” said Mike Mustapha, president of ABB electrification’s smart buildings division. “By combining digital energy management, efficiency improvements and renewable electricity, the team has delivered tangible reductions in energy use and emissions, while strengthening the competitiveness of the site. This is exactly the kind of progress we want to scale across our global operations.”
Beyond energy and emissions, Zibo has established a clear path toward circular operations. The site has implemented waste reduction and recycling initiatives and is targeting Zero Waste to Landfill certification under UL2799 by the end of 2026, reinforcing its commitment to responsible resource use and sustainable manufacturing. The facility joins a growing global network of ABB Mission to Zero sites spanning Europe, the Americas and Asia, all advancing toward low-carbon, energy-efficient and digitally enabled operations.
Even in autonomous systems, human insight is important Schneider Electric South Africa
IT in Manufacturing
As AI, IIoT and digital twins reshape industrial operations, Schneider Electric’s Kobus Vermeulen and Bafana Msibi argue that the operator’s role is shifting from controlling equipment to interpreting intelligence, validating AI recommendations and making decisions that improve
Read more...AI-based quality inspection scales across P&G operations Siemens South Africa
IT in Manufacturing
Siemens and Procter & Gamble are expanding an AI-based visual inspection system across P&G’s manufacturing operations worldwide, inspecting products in real time at full line speed, and reducing scrap rates by 10 to 20% depending on the product.
Read more...How sustainability unlocks real business impact Rockwell Automation
IT in Manufacturing
Sustainability has moved from a compliance obligation to a strategic driver of resilience and value for manufacturers. Rockwell Automation explains how its Triple A framework and connected-data approach help producers cut energy, water and waste while improving productivity.
Read more...Mining’s AI future will depend on people as well as technology
IT in Manufacturing
South Africa’s mining industry is embracing digitalisation and AI, but AvenirHoldings chief executive officer, Tshidi Mndzebele says the real test is whether the people behind the industry are equipped to move forward with it, and outlines five things mining needs to get right.
Read more...How BIC overcame operational silos to integrate technology and people Rockwell Automation
IT in Manufacturing
Manufacturing giant BIC deployed Plex MES from Rockwell Automation at its Bizerte plant in Tunisia, replacing fragmented, partly in-house software with a single cloud-based execution system that broke operational silos and improved shop-floor visibility.
Read more...AI in industry is an early warning system, not a guarantee Schneider Electric South Africa
IT in Manufacturing
Schneider Electric’s Paul Steyn argues that AI in industrial maintenance is only as good as the infrastructure and people behind it, and explains the three layers a facility needs before predictive maintenance can deliver on its promise.
Read more...SA’s mining industry must put people at the heart of its digital future
IT in Manufacturing
South Africa’s mining industry employs around 470 000 people while its digital transition accelerates. Avenir’s chief executive officer, Tshidi Mndzebele argues that technology should enable and upskill the workforce rather than replace it, setting out five ways mining can make technology work for its people.
Read more...Quality control supports efficient tissue production Valmet South Africa
IT in Manufacturing
Valmet’s advanced quality control technology is helping tissue producers improve product consistency while reducing energy and raw material consumption. Its latest installation at KORO Paper in Vietnam combines real-time measurement, process optimisation and non-contact, nuclear-free quality control.
Read more...Patented algorithm maximises operator efficiency Rockwell Automation
IT in Manufacturing
Rockwell Automation piloted a patented anomaly detection algorithm and FactoryTalk DataMosaix at its Twinsburg electronics plant, giving operators 30 to 60 days’ advance warning of stencil failure, improving fail rates by 22% and achieving a 200% return on investment.
Read more...Cybersecurity must become part of the next era of industrial automation Adroit Technologies
IT in Manufacturing
The EU’s Cyber Resilience Act is setting a global benchmark for connected products, making cybersecurity a core engineering requirement in industrial automation. Adroit Technologies and Mitsubishi Electric explain how building security into controllers, PLCs and drives from the outset helps South African manufacturers protect production and meet international expectations.
While every effort has been made to ensure the accuracy of the information contained herein, the publisher and its agents cannot be held responsible for any errors contained, or any loss incurred as a result. Articles published do not necessarily reflect the views of the publishers. The editor reserves the right to alter or cut copy. Articles submitted are deemed to have been cleared for publication. Advertisements and company contact details are published as provided by the advertiser. Technews Publishing (Pty) Ltd cannot be held responsible for the accuracy or veracity of supplied material.





 printer friendly version