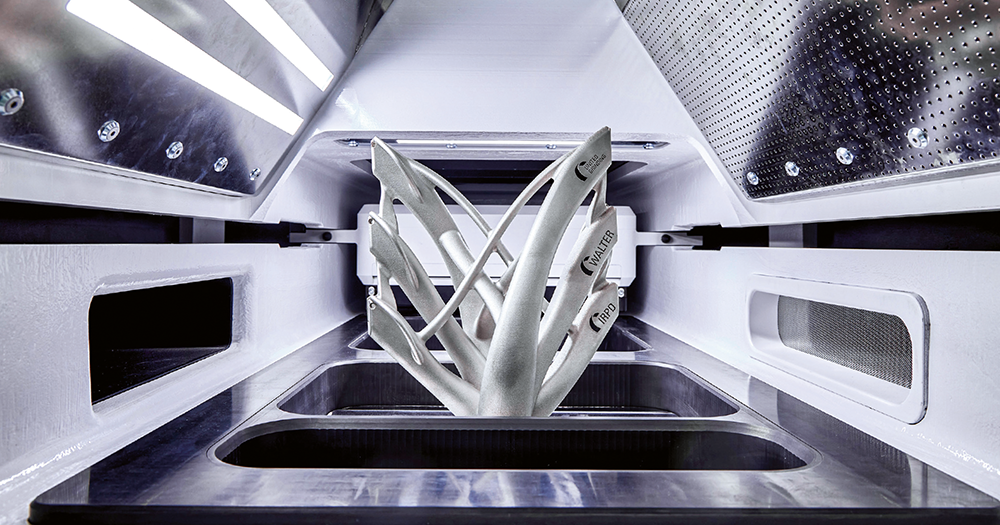
The main customer segments of the parent company, UNITED MACHINING SOLUTIONS and also the areas of application for the additive machine tools are automotive manufacturers and suppliers, as well as the aviation industry and cutting tool manufacturers. Stefan Lang, CEO of IRPD, explains: “In additive manufacturing, parts often have to be reworked at connection surfaces. Our parent company supplies the appropriate systems for this, which facilitates the vertical integration of the production process and offers the customer an end-to-end solution.” Dr Kai Gutknecht, head of process and software development at IRPD, adds: “In our target markets, the main priority is ensuring an efficient process from beginning to end. Accordingly, machine development specifically focused on achieving a high number of produced parts and ensuring consistently high quality. This starts with the large build area, the four 1000 W fibre lasers, and the container concept designed for fast job and material changes. It extends to the thermally and mechanically stable production environment, preparation for automation, and complete monitoring of the production process.”
LPBF system with machine tool standard
At the heart of the IMPACT Fab complete system is the IMPACT 4530 machine tool for the additive manufacturing of metal parts. Laser powder bed fusion (LPBF) enables the flexible production of high-quality parts from a wide variety of metals. In addition, there is the PM1 depowdering and recycling system which removes the remaining metal powder from the build container, sieves it under inert conditions, and transports it to the powder container for future tasks. Other system components include the LS1 loading station which is used to lift the build plates out of the container, and the HM1 handling module which moves the containers between the individual production stations.
The IMPACT 4530 itself consists of two main components: the machine core for the actual additive manufacturing process, and the supply unit for preparing various media. Dominik Lenherr, software engineer for automation at IRPD, explains the process flow: “The machine core is largely designed as a cast construction to ensure a stable and reproducible process, both thermally and mechanically. The machine is set up using two cube-shaped containers: one for the build process, and the other for storing the metal powder as the starting material. The automated insertion and docking of the containers speeds up and standardises the setup process, resulting in minimal downtimes, and allowing the start of a build job to be reproduced.”
Once the containers are hermetically docked in the machine, a high-quality process atmosphere is created in a time-efficient manner. A horizontal axis then applies metal powder layers to a build plate. These layers are then melted by several lasers and welded to the desired component cross-section. After lowering the build plate by a layer thickness of typically a few hundredths of a millimetre, new powder is applied and the process is repeated. According to Gutknecht, the key components here are the lasers and the galvanometer scanners which can be used to move the laser beam quickly and with micrometer precision. The system is rounded off by various monitoring solutions and the intuitive CORE (Customer Oriented Revolution) operating software used on all UNITED MACHINING SOLUTIONS machines which communicates with the Beckhoff TwinCAT control system via a simple, high-performance ADS interface.
Requirements for automation
As Lang explains, the starting point for the project was ideal when it came to choosing suitable automation technology: “As the IMPACT project opened up a completely new technology sector for IRPD, the control platform could be selected to meet the specific requirements of additive manufacturing. The system openness, the advanced development environment and the innovative products from Beckhoff were all arguments in favour of PC-based control with TwinCAT. Added to this was the PC-based control approach itself which opens up interesting possibilities with regard to a lean, easily expandable overall system architecture.”
PC-based control from Beckhoff controls all hardware-related machine functions in the IMPACT 4530, except for the movement of the laser over the powder bed. These functions include mechanical axes, pneumatics, machine safety, inert gas circulation, and cooling. The hardware core of the control system is the C6675 control cabinet industrial PC. Gutknecht explains: “One of our goals was to create a system architecture with low-threshold interfaces, and as few of them as possible. The basis for this is a powerful central system that maps the control and high-level language software on one piece of hardware, the C6675. We are not yet making full use of its high computing power, although the PLC, the vision application, and the resource-intensive CORE application are already running on it alongside Windows. Further applications such as process monitoring via cameras, big data, machine learning applications and additional process controls will be added in the course of further development.”
From IRPD’s point of view, the application-oriented approach to solving automation tasks was also very well supported by the modular TwinCAT software. TwinCAT Vision was used to quickly and easily integrate a camera for process monitoring into the control system. In addition, according to Lenherr, executing the image processing algorithms directly within the control environment makes it possible to capture image data with precise timing and in sync with the machine sequences, without having to set up and maintain complex interfaces. He adds: “The TwinCAT libraries such as TwinCAT HMI, motion, and even vision, provide comprehensive support with their ready-made function blocks for programming, commissioning and diagnostics of the various software components. I see integrated troubleshooting and analysis in particular as one of the biggest advantages of TwinCAT engineering. With TwinSAFE, machine safety is also seamlessly integrated, so we don’t have to work with different tools and only have to maintain one piece of software.”
Efficiency in motion control and EtherCAT communication
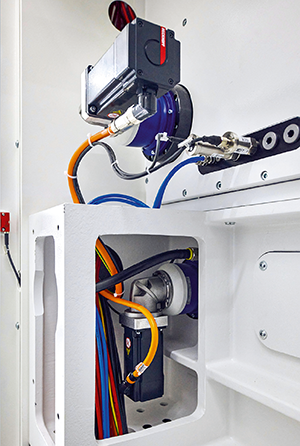
According to Gutknecht, IRPD also benefits from the TwinCAT function blocks when it comes to motion control: “We use the standard functions MC_MoveAbsolute, MC_Jog and MC_Reset, among others, which significantly reduces the programming effort for us. The associated servo axes are implemented with the very compact AX8000 multi-axis servo system and AM8000 servomotors. The One Cable Technology (OCT) offers us particular advantages as it simplifies the system cabling considerably and reduces the risk of errors during installation. In addition, our system is easy to take apart for transport, with the minimised cabling saving a lot of time when separating the parts.”
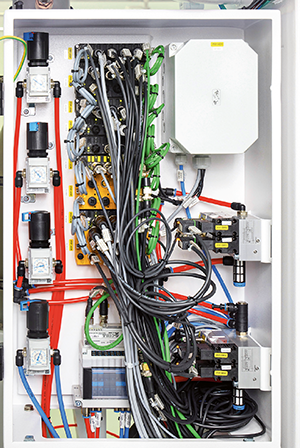
The high-performance EtherCAT communication also contributes to system efficiency, especially during commissioning. Lenherr explains: “A good example of this is EtherCAT’s hot connect functionality which we use for a coater, for example. The coater is available in a version with and without a drive controller and can be replaced quickly and easily via hot connect if required, without having to shut down the entire system or interrupt any necessary diagnostics.” Together with automatic device addressing, this also comes into play with regard to the modularity of PC-based control. For example, if requirements change, a higher-level controller can simply be added via the EP series EtherCAT Box modules with an IP67 protection rating, without the need for complex addressing. With regard to the Beckhoff I/O portfolio, he concludes: “A clear advantage of the EtherCAT I/Os from Beckhoff is their compact design, which saves a lot of space in the system. Added to this is the extremely wide range of components, which we could not find anywhere else on the market. Good examples include the multifunction EtherCAT Box modules with their combined analogue and digital inputs and outputs plus the TwinSAFE Box modules for the direct connection of field sensors for safety functions.”
| Tel: | +27 11 795 2898 |
| Email: | [email protected] |
| www: | www.beckhoff.com |
| Articles: | More information and articles about Beckhoff Automation |






© Technews Publishing (Pty) Ltd | All Rights Reserved
 printer friendly version