



When it comes to equipment maintenance and facility shutdowns, particularly for the oil and gas sector, saving even a single day can result in significant cost reductions. Key to ensuring that a schedule is completed on time, or sometimes accelerated, is having the right planning, people and equipment in place. Mammoet supported a leading Canadian energy provider in Alberta’s oil sands with replacing its original eight coke drums at its base plant site in Fort McMurray. The project would extend the life of the original upgrader by 30 years.
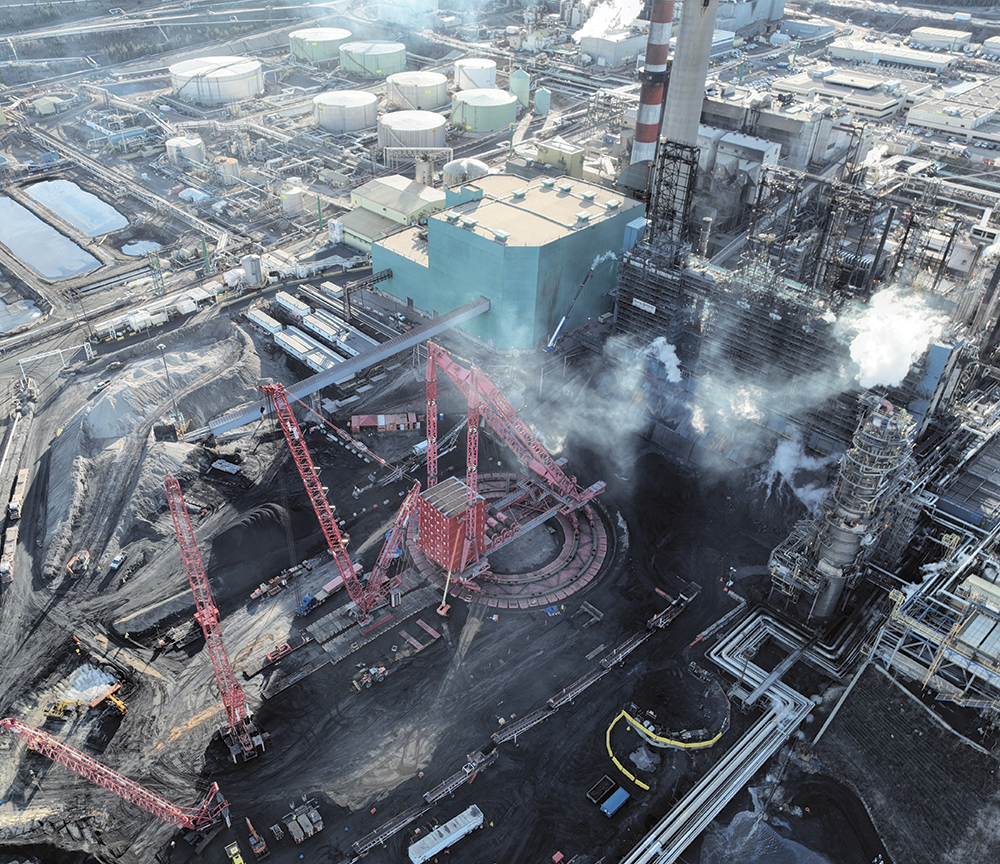
The site upgraders use thermal and chemical processes, including coking and hydrotreating, to convert bitumen into synthetic crude oil. Coke drums gather the petroleum coke that is separated from the feedstock during the refining process. Weighing 270 tons a piece, each coke drum is 7,9 m in diameter and 29,8 m high. Moving them into place required one of the largest cranes in the world.
Through early involvement, Mammoet was able to advise on the right crane for the job, and when one of the new components was heavier than estimated, they fabricated specialised rigging for the lift. The team also helped accelerate the schedule by shortening the time between two of the biggest lifts of the project, helping enable the upgrader’s early return to operation.
Choosing the right tools for the job
Mammoet was brought in during the planning stages to conduct a feasibility analysis, assess which equipment would be best to remove the old drums, and get the new ones delivered to site and installed.
“In terms of the importance of the project and getting everything done within a specific timeline, this turnaround was completed safely, ahead of budget and schedule,” explains Kurt Reid, sales manager at Mammoet. “With the daily cost being significant, it was essential that planning happened years in advance”.
Mammoet was an integral part of the project for over seven years prior to execution, discussing the timing of lifts and movements. Its engineers undertook an entire crane review, assessing every suitable model in Mammoet’s fleet to select the right equipment. The biggest consideration wasn’t weight, but reach.
The engineering team first considered using an LR 11350 crawler crane placed beside an upgrader wall, but the option wasn’t feasible because it interfered with concurrent operations and maintenance work in the area. Mammoet’s PTC210DS ring crane was chosen for its ability to lift the six-drum derrick weighing over 1200 tons. Its long reach also allowed assembly away from other ongoing work. As the PTC had to be erected inside the coke pit, civil work was needed to strengthen the ground beneath it. Around 200 piles were driven into the ground to build a solid foundation.
Getting everything ready and in place
Prior to project execution, the new components were delivered to site. They were transported from their fabricator in Edmonton to Fort McMurray using prime movers on Alberta roads, and self-propelled modular transporters (SPMTs) on site.
This process started a year and a half before the project area would shut down for execution. Niek de Winter, corporate account manager at Mammoet, explains why. “Our plan was to ensure that all necessary equipment, materials, and components were delivered to the site by December of the previous year. This approach would allow the turnaround process to commence promptly and without delay upon the scheduled plant shutdown on 1 May.The crane was assembled, the coke drums and derricks were on site, everything was there months ahead of time. This allowed us to eliminate delays mid-project”.
On site, two sets of SPMTs and crews allowed things to move forward continuously and the PTC crane to be constantly fed.
Using the PTC to save time and cost
The old derricks were lifted first, followed by the eight coke drums and finally their concrete foundation sections. The old components were placed onto SPMTs and driven to a nearby laydown area for decommissioning. For the installation of the new components, the process then happened in reverse.
The fourth deck derrick ‘supermodules’ were transported to the facility in smaller modular sections and then moved and assembled on site. The base of these supermodules made up the operating deck of the coke drums and were assembled via SPMT from the smaller modules. The derricks were erected with Mammoet crawler cranes.
Due to a weight increase of the largest derrick supermodule, the project team at Mammoet had to maximise use of the PTC210 to deliver the needed lifting capacity. It was reconfigured with a double masthead kit, and specialised rigging was also fabricated.
Accelerating the schedule
Thanks to detailed planning, specialised equipment and the disciplined approach, production at the site could continue right up until 30 April, the day before the shutdown. From factory to foundation, Mammoet safely and efficiently managed its components on site ahead of the turnaround.
“As soon as we are called on, we are ready to perform the next lift. When you have a client that is planning their multi-week event right down to 15-minute intervals, time is of the essence,” concludes Reid.
For more information contact Jana Wolf, Mammoet, [email protected], www.mammoet.com






© Technews Publishing (Pty) Ltd | All Rights Reserved
 printer friendly version