



There are few qualities so desirable for a business to have than an ability to adapt to change. Industries evolve, circumstances shift, but what remains over time are those businesses with the foresight and flexibility to move with the tides.
Such adaptability is perfectly exemplified by limestone calciner Singleton Birch. Formed in 1815, the company has endured through multiple industrial eras and continues to thrive to this day. In part, this is due to the company’s unique structure. Governed by a board of trustees composed of several charities along with descendants of the original owners, the company has a devout focus on reinvesting capital back into the organisation to fuel continual improvement and modernisation initiatives. It’s this approach that has given the Lincolnshire-based company the flexibility to deliver an expansive set of products and services to more than 300 customers, across the energy, utilities, water treatment and steel sectors.
Command and control
A central component for managing this complex supply chain is its control operations. This function is responsible for monitoring everything from the extraction of calcium carbonate (limestone) through to delivery of products and removal of wastes at remote customer sites. Historically, command operations were managed via eight separate control rooms, situated in proximity to production locations, each with its own operational and engineering staff. These locations incorporated around 40 legacy PLCs and 25 scada applications, each supported by separate servers at the remote locations.
The company was experiencing limitations with this approach. The operations were siloed, and there was little coordination between activities in separate parts of the operations: such as the quarry, kilns and production plants. This presented issues from a resource allocation perspective, and also created safety risks due to fractured communications between the sites. The approach was also costly due to the need to operate multiple different sites and have staff present in each. Additionally, there was an ongoing risk of downtime due to a lack of redundancy in the company’s IT infrastructure. This could be a major issue if one of the control rooms did experience downtime, as it would be inoperative for hours – and possibly days – while engineering work was arranged.
Acknowledged as an area for improvement, the company began the process in 2015 of consolidating and integrating its control operations. The initiative aimed to replace the multi-site approach with a single control room with complete visibility across the company’s entire operations. Working with its longstanding systems integrator, InControl Systems, the board saw the project as an opportunity for cost saving and competitive advantage. Following a discovery workshop in 2017, it approved the development of an integrated control centre, supported by a new, on-premise data centre.
The vision for the project also aligned with a broader organisational push to adapt the company culture and integrate its production chain. This meant moving away from fragmented, generalist staff managing different parts of company operations, towards fully integrated operations via specialist operators. The new control centre would become a state-of-the-art facility with duties ranging from resource allocation and optimisation, through to safety and logistics, with the twin goals of cost reduction and value addition.
InControl Systems helped compose a team of expert technology providers, including Rockwell Automation, PTC and InVMA, to bring the vision to reality.
Transforming from the centre
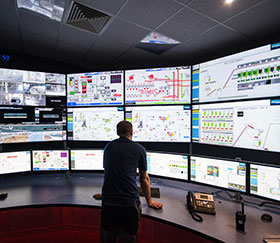
Beginning the installation phase in May 2019, it took eight weeks to build the control room. The process involved installing more than 40 large screens, redundant servers and support applications, connected to PLCs using control logic gateways on an Ethernet network. These screens would give operators the flexibility to monitor across operations using a single log-on, with minimal maintenance.
To support the new control centre capabilities, Singleton Birch created an adjacent data centre with the objectives of creating greater redundancy and improved data quality. In this data centre it installed two Rockwell Automation FactoryTalk View SE unlimited redundant client server architectures, one for quarry operations and one for process operations, which helped them to significantly minimise downtime. A redundant ThinManager configuration was also implemented to ease the process of managing such a large array of screens and simplify the associated maintenance. Finally, FactoryTalk AssetCentre was installed to provide total audit and improve traceability of software modifications.
The data centre also included PTC ThingWorx and Kepware solutions, which allowed operators to stitch together data from multiple sources, including the control systems, energy monitoring, CRM and planning systems. This provided operators with important insight into stock and production data in order to enable more accurate forecasting of manufacturing and delivery requirements.
By August 2019 the new system was completely functional – the quick project turnaround aided by the flexibility and scalability of the ThingWorx platform. With their new-found capabilities, operators gained clear visibility over equipment effectiveness, maintenance management systems and financial information. The integrated system brought operators and engineers closer together, meaning that maintenance tasks could be operationalised. The setup also functionally separated control operators from on-the-ground supervisors. The control operators would act as the supervisors’ ‘eyes and ears’, analysing data and providing recommendations to the remote locations.
Integrated working
In the time since the control centre became operational, the new capabilities have become an important part of Singleton Birch’s plant operations. At a technical level, the centre’s impact has aligned well with the board’s strategic intent. Key benefits have included:
• Improved availability: availability has improved by more than 20% due to system efficiencies, massively decreasing instances and impact of system faults.
• Reduction in energy consumption: the system includes sub-metering so that operators have granular insight and greater control over manufacturing and energy consumption across the plant.
• Improved cost and flexibility: the cost of operation has been reduced by around 13%, taking into account the price competitiveness of the solution and the reduction in personnel required to maintain operations.
• Improved safety: supervisors are now remote from physical operations, meaning they are able to identify issues earlier and benefit from having engineers in closer proximity for proactive maintenance.
• Better management and integration: the centralised nature of the control centre has supported the project’s overarching objective of establishing better levels of visibility and joined-up decision-making across site operations.
• Sales and revenue generation: the new system allows Singleton Birch to gain better control over the various aspects of its supply chain, supported by enhanced logistics. This approach has helped to differentiate the company’s business model and boost its competitiveness.
• Cultural improvement: the control operation staff have been engaged in the process from day one. They now work in a more comfortable environment with better equipment. They have also benefitted from an improved flow of decision-making and efficiency, meaning they can act in real time to emerging issues.
Looking to the next two centuries
The project’s success epitomises the ethos that has held Singleton Birch in strong standing over its 200-year history. The strategic process of identifying an area for improvement, piloting solutions and executing on the plan lays the blueprint for ongoing organisational improvement. The integrated control centre project has not only helped the company to run its plant in a much more efficient and cost-effective manner, but is also producing cultural benefits that it anticipates will translate into greater staff engagement and career advancement.
This transformation has been made possible by the support of its partners, including Rockwell Solutions, which have shown a keen understanding of the company’s principles and ambitions. Lending their expert advice on the portfolio of advanced, complementary systems available, the project team have worked together to apply these tools in practice.
Staying true to its roots, while displaying the courage to transform, puts Singleton Birch in control of its future.
| Tel: | +27 11 998 1000 |
| Email: | [email protected] |
| www: | www.rockwellautomation.co.za |
| Articles: | More information and articles about Rockwell Automation |






© Technews Publishing (Pty) Ltd | All Rights Reserved
 printer friendly version