Energy costs eating into bottom line? Add IoT
Technews Industry Guide: Industrial Internet of Things 2017
IT in Manufacturing
Double digit increases in the cost of electricity since 2006 have eaten into corporate and industry profitability and was listed by Business Times as a contributing factor in the decline in business confidence in 2016.
Using the Internet of Things (IoT) technology can deliver efficiencies and cost savings that can, to a large degree, offset the profit-eroding impact of continued price escalation.
“In the wake of rapid price increases companies have initiated a number of projects to improve energy efficiencies with some success. Implementing an IoT strategy can be the differentiator,” says André Strauss, director of partnerships at Pretoria-based technology company IoT.nxt.
“Some executives are hesitant to introduce IoT solutions because of the perceived cost of additional capital expenditure. This is not required. The implementation of IoT strategies gives companies crucial insight into power usage, which allows them to manage their tariff range in real time. Having insight and control over their tariff range thresholds and consumption, turns this profit-drain into informed decisions with real-time benefits,” he adds.
The website European Energy Innovation reported late last year that the IoT can bring significant benefits for energy efficiency. “At the level of the production of energy, smart grid sensors can improve utility operations and performance by better monitoring the energy network, so that resources are allocated more precisely and closer to the actual demand needs, avoiding energy waste. At the level of consumption, smart meters can provide a wealth of information to help minimise energy costs, e.g. through fully automated billing based on time of use or network status, or enabling meter-to-appliance communications to help consumers change their behaviour to reduce their costs,” according to a report on the site by Mário Campolargo, director for the Net Futures department of the European Commission.
Strauss lists seven benefits of energy consumption and monitoring:
• Information gathered provides a 360 degree view of where energy is lost, misused or even stolen.
• Energy load and disturbance management to detect problems before they happen.
• It creates organisational awareness about energy management.
• Facility managers can use the information to optimise energy without wasting spend.
• Information about energy utilisation over a period of time proves valuable insight for an alternative energy strategy.
• Effective carbon footprint management to conserve energy as well as the environment.
• Cost reduction so companies can save money and energy.
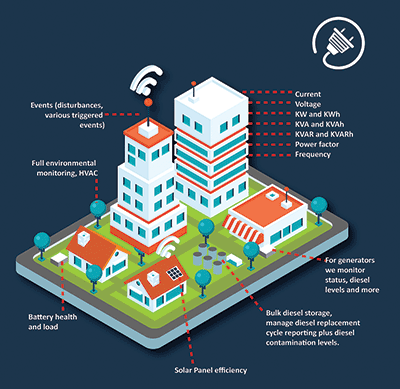
“The IoT.nxt Raptor edge gateway integrates monitoring capability to monitor far more than the traditional elements of energy processes and assets. This allows a company to monitor every variable in its operational chain, providing a comprehensive real-time, situational context of every element in its energy landscape. The Raptor was designed with interoperability in mind,” explains Strauss.
IoT.nxt is in the final stages of developing this application for a large regional shopping mall in Gauteng, where energy charges are a key cost factor. “Lighting and air conditioning contribute the biggest percentage of the total energy cost at this mall. Once installed our solution will bring costs down significantly,” he adds.
At large manufacturing plants, mining, utilities management by cities, and several other industries, the energy efficiency solution could be integrated into a larger IoT project where different elements are managed better through real-time monitoring, delivering even greater costs savings.
For more information contact Daleen van Wyk, IoT.nxt, +27 (0)83 302 0827, [email protected], www.iotnxt.com
Further reading:
Even in autonomous systems, human insight is important
Schneider Electric South Africa
IT in Manufacturing
As AI, IIoT and digital twins reshape industrial operations, Schneider Electric’s Kobus Vermeulen and Bafana Msibi argue that the operator’s role is shifting from controlling equipment to interpreting intelligence, validating AI recommendations and making decisions that improve
Read more...
AI-based quality inspection scales across P&G operations
Siemens South Africa
IT in Manufacturing
Siemens and Procter & Gamble are expanding an AI-based visual inspection system across P&G’s manufacturing operations worldwide, inspecting products in real time at full line speed, and reducing scrap rates by 10 to 20% depending on the product.
Read more...
How sustainability unlocks real business impact
Rockwell Automation
IT in Manufacturing
Sustainability has moved from a compliance obligation to a strategic driver of resilience and value for manufacturers. Rockwell Automation explains how its Triple A framework and connected-data approach help producers cut energy, water and waste while improving productivity.
Read more...
Mining’s AI future will depend on people as well as technology
IT in Manufacturing
South Africa’s mining industry is embracing digitalisation and AI, but AvenirHoldings chief executive officer, Tshidi Mndzebele says the real test is whether the people behind the industry are equipped to move forward with it, and outlines five things mining needs to get right.
Read more...
How BIC overcame operational silos to integrate technology and people
Rockwell Automation
IT in Manufacturing
Manufacturing giant BIC deployed Plex MES from Rockwell Automation at its Bizerte plant in Tunisia, replacing fragmented, partly in-house software with a single cloud-based execution system that broke operational silos and improved shop-floor visibility.
Read more...
AI in industry is an early warning system, not a guarantee
Schneider Electric South Africa
IT in Manufacturing
Schneider Electric’s Paul Steyn argues that AI in industrial maintenance is only as good as the infrastructure and people behind it, and explains the three layers a facility needs before predictive maintenance can deliver on its promise.
Read more...
SA’s mining industry must put people at the heart of its digital future
IT in Manufacturing
South Africa’s mining industry employs around 470 000 people while its digital transition accelerates. Avenir’s chief executive officer, Tshidi Mndzebele argues that technology should enable and upskill the workforce rather than replace it, setting out five ways mining can make technology work for its people.
Read more...
Quality control supports efficient tissue production
Valmet South Africa
IT in Manufacturing
Valmet’s advanced quality control technology is helping tissue producers improve product consistency while reducing energy and raw material consumption. Its latest installation at KORO Paper in Vietnam combines real-time measurement, process optimisation and non-contact, nuclear-free quality control.
Read more...
Patented algorithm maximises operator efficiency
Rockwell Automation
IT in Manufacturing
Rockwell Automation piloted a patented anomaly detection algorithm and FactoryTalk DataMosaix at its Twinsburg electronics plant, giving operators 30 to 60 days’ advance warning of stencil failure, improving fail rates by 22% and achieving a 200% return on investment.
Read more...
Cybersecurity must become part of the next era of industrial automation
Adroit Technologies
IT in Manufacturing
The EU’s Cyber Resilience Act is setting a global benchmark for connected products, making cybersecurity a core engineering requirement in industrial automation. Adroit Technologies and Mitsubishi Electric explain how building security into controllers, PLCs and drives from the outset helps South African manufacturers protect production and meet international expectations.
Read more...










 printer friendly version