



Potash, a fine-grained mineral that contains potassium and is commonly used in food production, is in abundance in Saskatchewan, Canada. Mammoet has supported Ledcor with the construction of BHP’s new Jansen potash mine which is planned to begin production in 2027. It will become one of the largest potash mines in the world and is estimated to produce approximately 8,5 million tons per annum when it is fully operational.
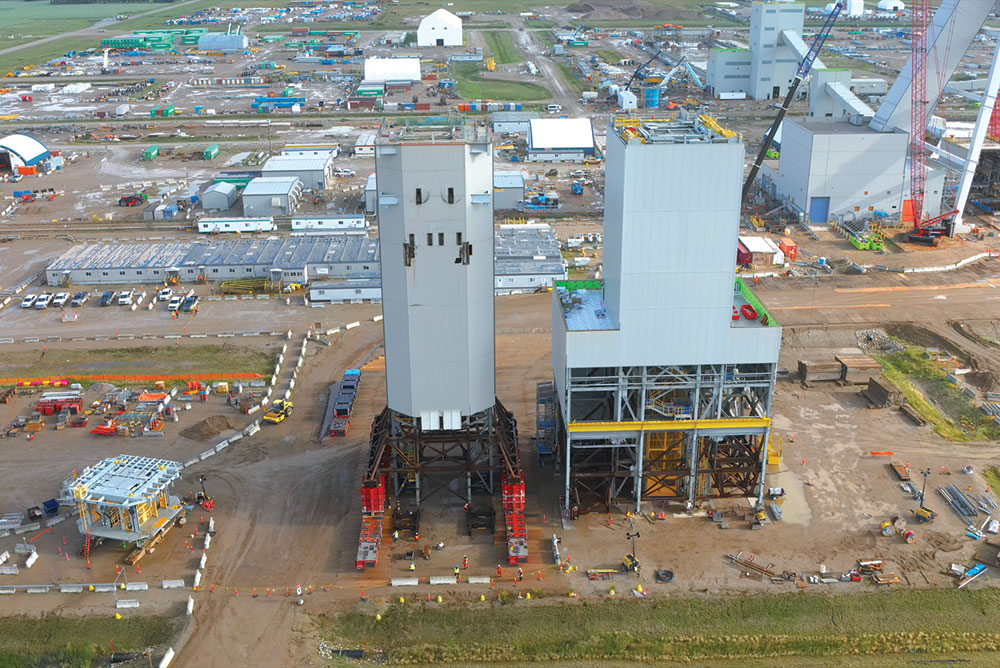
A mine’s headframe is positioned above the shaft, delivering people, equipment and materials below and above ground. The key scope for Mammoet was to remove the lower section of an existing headframe unit and replace it with a larger one to increase mining capacity.
Separately, it also supported with the complex lifting of a staircase tower module from inside the building where it was to be installed.
With Jansen’s remote location, modular construction techniques enabled the units to be prefabricated, delivered, assembled on site and installed efficiently. This approach, enabled by Mammoet’s heavy lifting and transport expertise, limited the amount of construction equipment and operators on site, and allowed parts of both components to be built in parallel, shortening the project schedule relative to other methods.
Planning collaboratively
The project had been in planning for many years. Mammoet’s introduction to it first started in 2013, when the original headframe unit was built. The modules for the new headframe were prefabricated at specialist facilities in the city of Edmonton and other places in the province of Alberta. The modules for the staircase tower were also built in Edmonton.
The parts were transported to the site on platform trailers fitted with transport beams. This phase wasn’t without its challenges, as Mike de Wilde, project manager at Mammoet, explains: “Jansen is mainly farmland, so you will often see agricultural equipment and machinery being transported on its roads, but shipping these large modules presented issues when staging our trucks overnight. We couldn’t just pull into a normal layby because the trucks would fill the entire area. The schedule had to be carefully planned and managed”.
During this planning phase, the ground condition on site was also an important consideration. During the spring the ground becomes soft and wet, so the team performed a ground-loading test between the laydown area and the mine shaft.
SPMTs carrying counterweights tested the route so that areas of potential sinking could be identified. As a result, more than 400 crane mats were mobilised because the ground was deemed too soft.
A section of ground by the shaft opening also needed to be reinforced to take the weight of the new headframe module. A shoring system, constructed of 21 metre towers was constructed at a basement level to provide stability. Due to the size of Mammoet’s global fleet, extra steel supports could be mobilised from its Dubai and United Kingdom yards, reducing overall risk levels despite the tough conditions.
The real heavy lifting begins
With the modules on site, the team began removing the existing headframe and prepared for the installation of the new one. A 22 axle line and 20 axle line SPMT combination, both fitted with steel supports, were driven underneath the 796 ton headframe module. The supports were necessary as using crane mats would have exceeded the ground-bearing pressure limits.
The SPMTs lifted the headframe using their onboard stroke, allowing Ledcor and BHP teams to remove the temporary steel supports, then the unit was driven to a laydown area.
Before the new headframe could be installed, Mammoet supported with the connection of a 60 ton staircase tower inside it.
An LR1300 crawler crane lifted in strand jacks and other equipment through an opening at the top of the building. The team then assembled the intricate winch system to lift the staircase tower.
The system comprised strand jacks and also spools to secure the 65 metres of cable needed to pull the staircase tower module from the bottom to the top of the building.
The removal of the original headframe unit left a large opening at the base of the building, enough space to manoeuvre the staircase module in range of the strand jacks using and LR1500 crawler crane. Once the unit was inside the building, its position was manually adjusted using pullies and chain hoists so it could be secured and lifted.
Adapting to challenges
The last phase of the project was the installation of the new headframe, which weighed 2090 tons, an almost 1300 ton increase from the previous headframe.
A configuration of two double SPMT trains, with a combined 80 axle lines were used for the movement. Finding the best configuration proved the biggest challenge.
“We had to find a trailer configuration where we could carry the additional weight, be under the permissible ground-bearing pressure, plus be short enough to not clash with the existing structure,” explains de Wilde. “Making this installation even more difficult was the fact that a section of the new headframe had to dock inside the staircase tower building. We were pretty much stroked out with the SPMTs, so it was a very tight fit. We had to align the head frame precisely with bolt positions specified in the engineering plans. Ledcor arranged for guidance lasers to be set up at the end of the platform and our SPMTs had to align with them perfectly, because every deviation could cause serious problems when it came to setting the module down. It was a very precise manoeuvre.”
This project demonstrates Mammoet’s skill when it comes to modular construction and efficient fabrication-to-foundation solutions. The option to use fabrication facilities and deliver everything to the site was a huge benefit in terms of schedule and cost efficiency.
A lot of specialised engineering went into making sure that everything arrived on schedule and was connected smoothly. This is where Mammoet excels, meeting the demands of its customers and delivering excellence in engineering, delivery and safety.
For more information contact Mammoet Global,






© Technews Publishing (Pty) Ltd | All Rights Reserved
 printer friendly version